Key takeaways
Every wind turbine blade, however long, is held onto the hub by a ring of bolts at its root. The blade can be perfectly molded along its full length, and if that bolt ring is drilled a little out of position, the blade will not fit, or it will fit and wear out its joint early. The final few hours a blade spends in the factory, cutting and drilling the root, decide whether all the hours before them pay off.
TurboMac is Cybernetik’s robotic root end machining system for wind turbine blades. It saws the root to length, removes the cut ring, mills the root face flat, marks and verifies hole positions, then drills the axial and radial bolt holes in one automated cell. Two models cover root pitch circle diameters from 2,800 mm to 4,800 mm and blades up to 100 m long, and Cybernetik states it cuts cycle time by up to 50 percent compared with special purpose machinery.
This article explains what TurboMac does, how the two models differ, what its accuracy figures mean in practice, and what a blade plant needs to have ready before installing one.
Why Root End Machining Needs Its Own Machine
The root of a blade is the thickest and stiffest part of the structure, a heavy laminate of glass or carbon fiber in resin. Cutting it is slow, abrasive work. Tools wear quickly, the cut creates a fine slurry, and the parts involved are enormous. A blade of 65 to 100 m has to be held still while a saw passes through a root that may be close to 5 m across.
At the same time, the accuracy needed is closer to that of a precision machine shop than a composites plant. The root face has to be flat, and dozens of bolt holes have to sit on an exact pitch circle and meet their cross holes inside the laminate. Few machines are built to handle both the size and the precision, which is why root end machining has traditionally been done on special purpose machines built for one blade family.
Root machining is one step in a longer chain that starts with layup and molding. Where it sits in the overall flow is covered in the guide to wind turbine blade manufacturing.
What TurboMac Does
Cybernetik describes TurboMac as a first-of-its-kind automation solution for accurate and rapid sawing, milling and drilling at the root end. It brings the full sequence into one cell, so the blade is referenced once and every operation works from the same datum.
The manual check before drilling is deliberate. Once a hole is drilled in a finished blade, there is no undoing it, so a short human check at that point protects hours of work. Each step, and what tends to go wrong in it, is explained in detail in the article on the wind turbine blade root.
The Two TurboMac Models
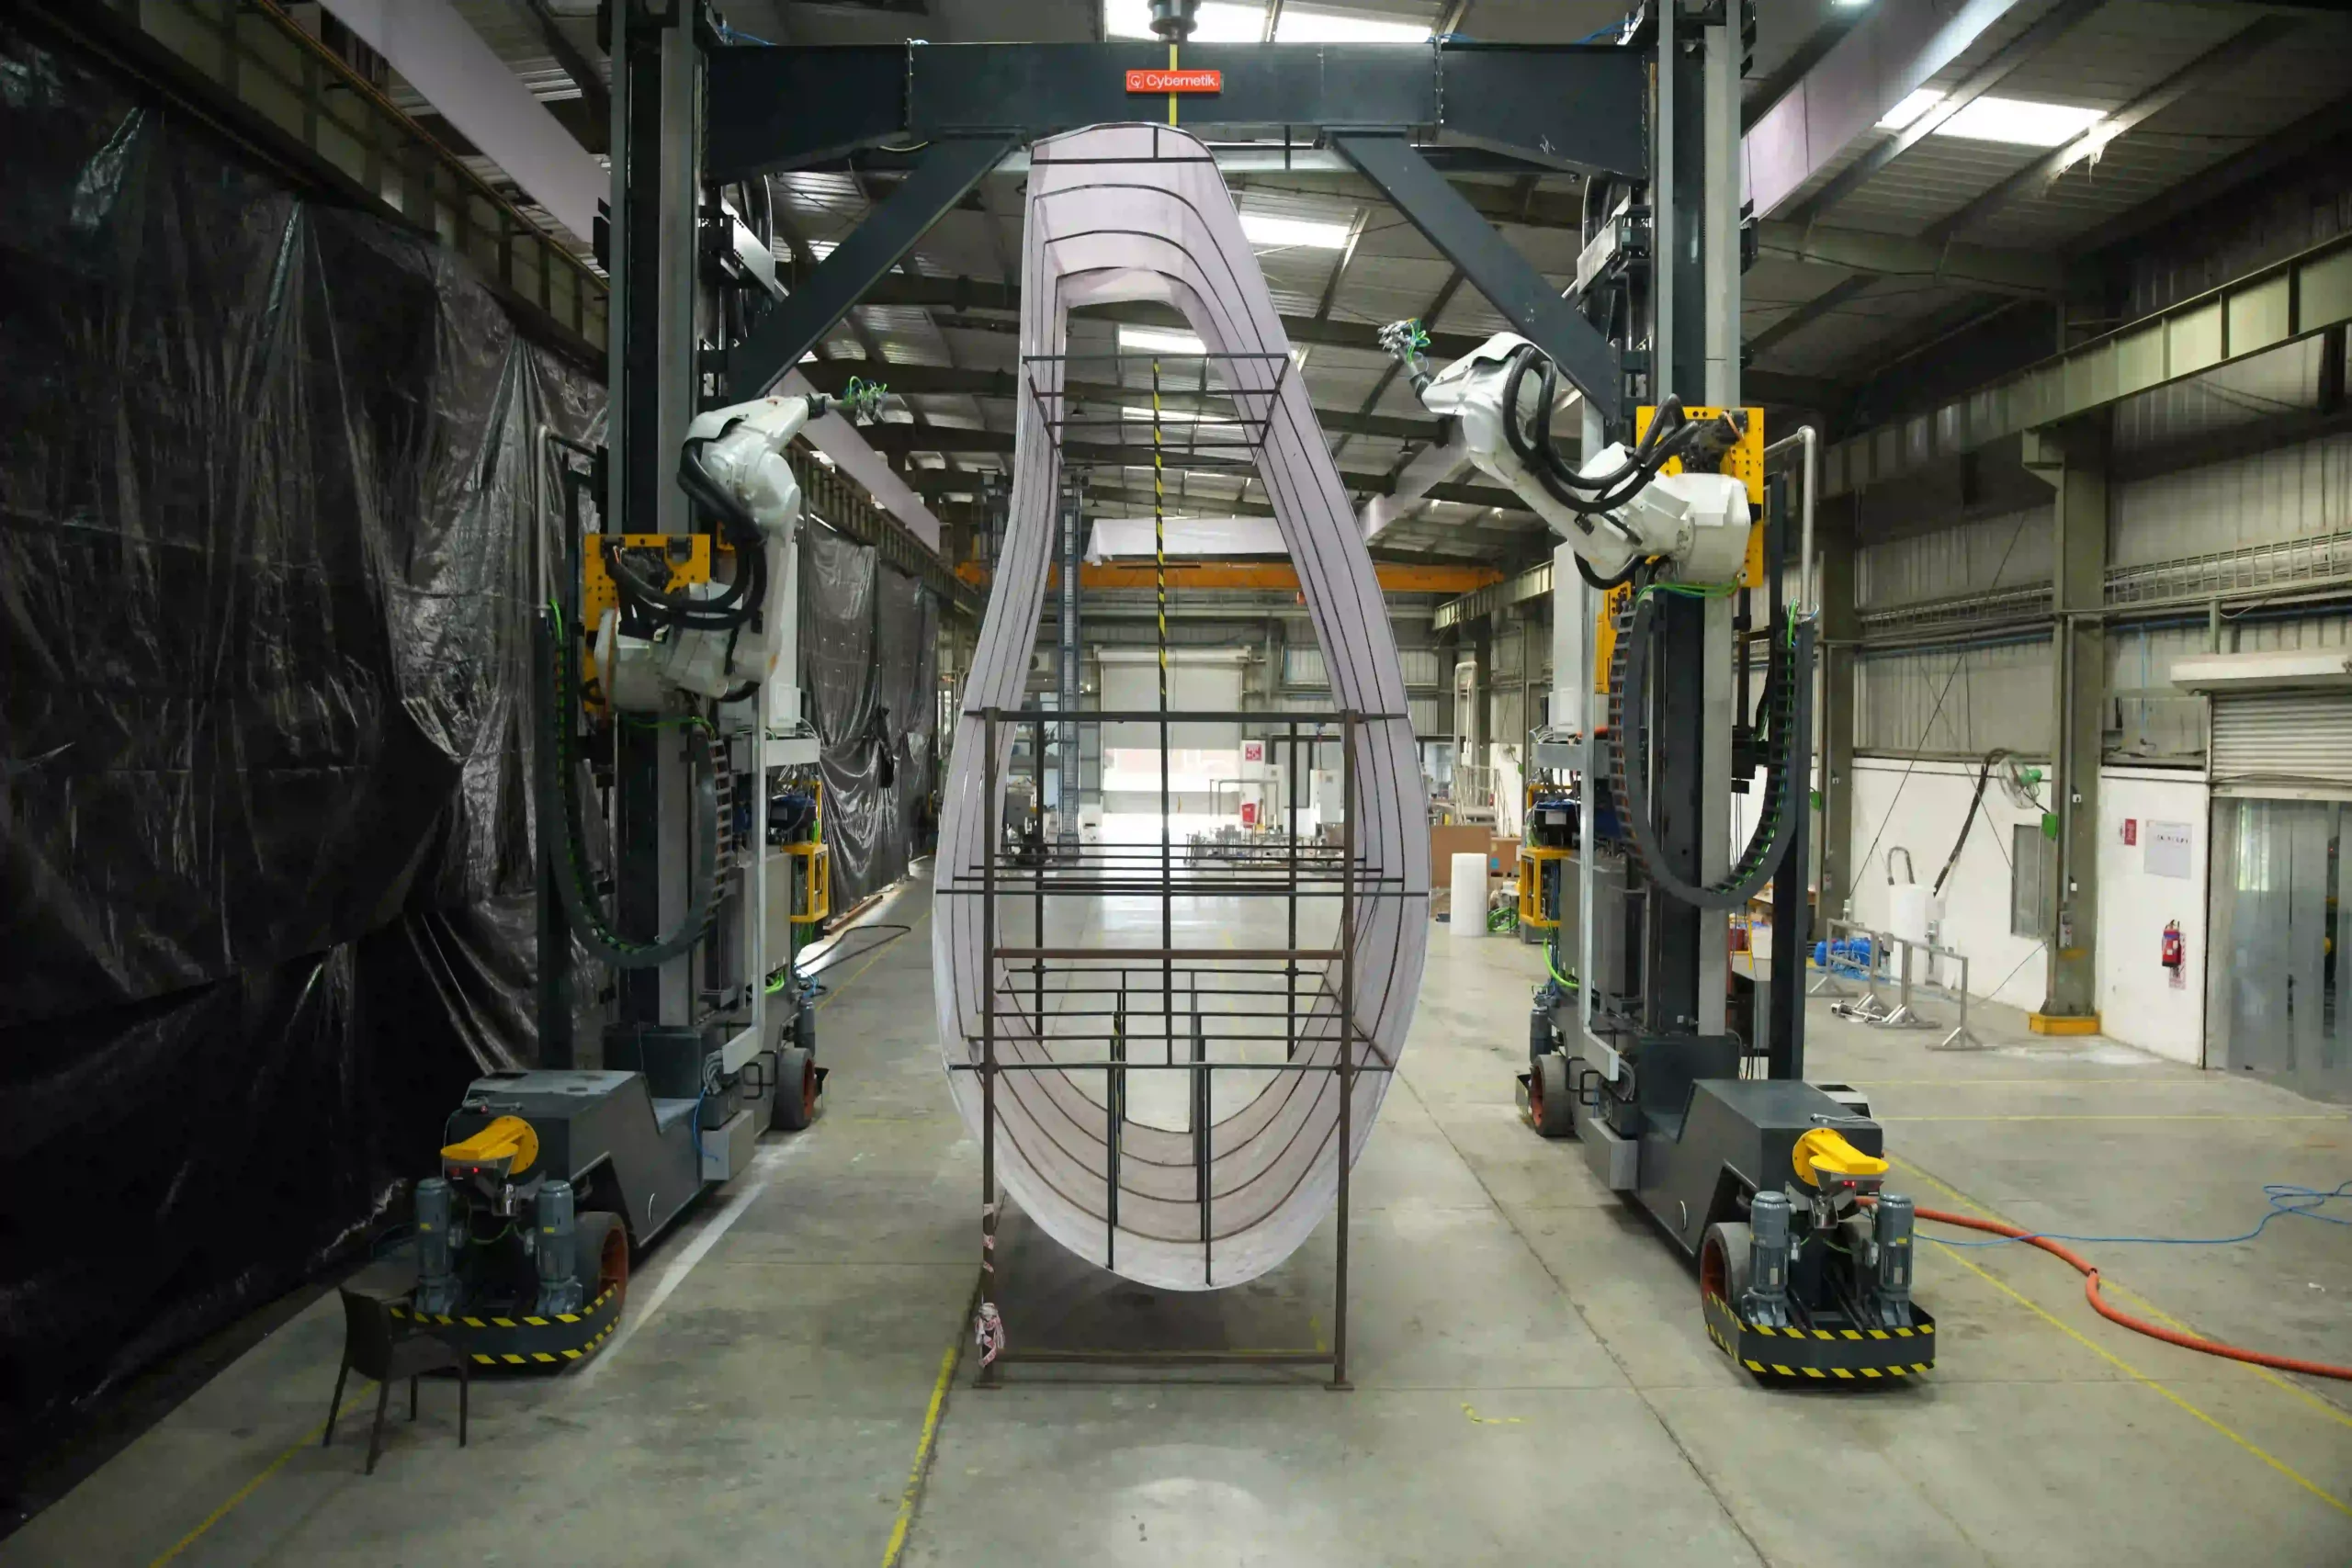
TurboMac comes in two sizes, set by the diameter of the blade root rather than by output. Both run at a similar pace and share the same footprint and utility needs, so the choice comes down to the blades you build now and the ones you expect to build next.
| Parameter | TurboMac 3000 | TurboMac 4800 |
|---|---|---|
| Root pitch circle diameter (PCD) | 2,800 to 3,000 mm | 3,000 to 4,800 mm |
| Blade length handled | 65 to 70 m | Up to 100 m |
| Throughput | About one blade every 8 to 10 hours | About one blade every 8 to 10 hours |
| Footprint | 15 x 8 m, customizable | 15 x 8 m, customizable |
| Electrical supply | 65 kW / 87 hp / 112 A, 415 VAC, 50 Hz, 3 phase | 65 kW / 87 hp / 112 A, 415 VAC, 50 Hz, 3 phase |
| Compressed air | 275 cfm at 6 bar | 275 cfm at 6 bar |
| Standards | CE and UL compliant | CE and UL compliant |
Choosing between them
The TurboMac 3000 suits plants building blades in the 65 to 70 m range, with roots up to 3,000 mm across. The TurboMac 4800 covers roots from 3,000 mm up to 4,800 mm and blades up to 100 m, which is where larger onshore and offshore platforms are heading.
Blade lengths have grown steadily, and a plant that builds 70 m blades today may be quoting for longer designs within a few years. If that is likely, it is worth discussing whether the larger model, or the flexibility for PCD and layout changes that both models offer, better protects the investment.
It also helps to look at the bolt layouts you machine, not just the diameter. Two blades with similar roots can use different hole counts, hole depths and radial positions. Sharing the full root drawings for current and planned blades at the start lets the configuration be checked against every layout the cell will see.
What the Accuracy Figures Mean
Specification sheets list tolerances, but it helps to know what each one is there to prevent. The figures below are Cybernetik’s published values for the TurboMac 3000, with a plain explanation of why each matters at the hub.
| TurboMac 3000 specification | Value | What it protects |
|---|---|---|
| Milling flatness (on blade) | 0.500 mm | Even contact between the root face and the pitch bearing, so the bolt preload is shared evenly |
| Radial hole to milling plane parallelism (on mandrel) | Under 0.250 mm | Radial holes that sit square to the face, so barrel nuts seat correctly |
| Axial hole to milling plane perpendicularity (on mandrel) | Under 0.25 mm | Bolts that run straight into the hub instead of bending under load |
| Intersection of radial and axial holes (on mandrel) | Under 0.250 mm | Each bolt meeting its barrel nut cleanly, with full thread engagement |
| Axial hole PCD (on blade) | 3000.000 ± 1 mm | A bolt circle that matches the hub, so the blade fits the first time |
Note the difference between values measured on the blade and those measured on a mandrel. The mandrel figures describe how precisely the cell positions and drills, measured on a reference part. The on-blade figures describe what is achieved on the actual composite root, which is the result the turbine maker will check.
A pitch circle of 3000.000 ± 1 mm on a 3 m root is tight for a composite part this size. Holding it depends on referencing the real blade rather than the drawing, and on keeping the spindle stable as it warms up through a long cycle, which is where some of TurboMac’s features come in.
Robotic Cell Versus Special Purpose Machine
Most blade plants that machine roots today use special purpose machines, built around a particular blade family. They work, but they can be rigid when a new blade design arrives. TurboMac takes a robotic approach instead, and the main differences show up in cycle time, flexibility and the support systems around the cut.
| Special purpose machine (SPM) | TurboMac robotic cell | |
|---|---|---|
| Cycle time | The reference point | Up to 50 percent shorter, as stated by Cybernetik |
| New blade PCD or bolt layout | Often needs mechanical rework or new tooling | Flexibility for changes in PCD, layout and robot functionality |
| Process data | Varies by build, often limited | Sensor-based process optimization, data logging and condition monitoring |
| Slurry from cutting composite | Usually sent to an effluent treatment plant | Slurry drying system that removes the need for an effluent treatment plant |
| Spindle temperature | Depends on the machine | Chilling unit holds spindle motor temperature |
| Sawn-off ring | Often handled with cranes and manual effort | Built-in ring removal system |
The cycle time figure is the one most plants ask about first. Root machining often runs at the end of the blade line, so if it is slower than molding, finished blades queue in front of it. Shortening that step can raise the output of the whole line without adding another mold.
Features That Keep the Cell Running
Slurry drying
Cutting composite with coolant creates a slurry of resin and fiber particles. Many plants send it to an effluent treatment plant, which adds cost, space and compliance work. TurboMac includes a slurry drying system that Cybernetik states removes the need for an effluent treatment plant for this waste.
Spindle temperature control
A spindle that heats up through a long cycle grows slightly, and that growth shows up as position error in the last holes drilled. A chilling unit keeps the spindle motor at a steady temperature, so the final hole on the pitch circle is drilled under the same conditions as the first.
Ring removal
The ring sawn from the root is heavy and awkward to move. A built-in ring removal system clears it safely and quickly, so the cell can move straight on to milling instead of waiting for manual handling.
Data logging and condition monitoring
Sensor-based process optimization, data logging and condition monitoring give a record of each blade and early warning of wear on tools and drives. Cybernetik also lists improved surface finish and longer tool life among the benefits. That kind of data link is part of a wider move toward connected renewable energy automation across component plants.
 “As wind turbine blades grow larger and designs continue to evolve, manufacturers need machining systems that combine precision with flexibility. Robotic automation helps accommodate changing root dimensions and bolt layouts without the limitations of rigid, blade-specific machinery.”
See it in action
Preparing a Plant for TurboMac
A root machining cell is a large installation, and most delays in projects like this come from the site rather than the machine. These are the items worth settling early.
| Site item | What to plan for |
|---|---|
| Floor space | A 15 x 8 m cell footprint (customizable), plus room to bring the full blade in and out |
| Power | 65 kW at 415 VAC, 50 Hz, 3 phase, 112 A |
| Compressed air | 275 cfm at 6 bar, on top of what the rest of the blade shop already uses |
| Blade handling | Cranes or transport fixtures that can present the blade root to the cell |
| Dust and slurry | Extraction and space for the slurry drying system and dried waste |
| Tooling and spares | Stock of saw blades, milling cutters and drills sized for composite wear |
| Data connection | A link from the cell to the plant network so logged data reaches quality records |
Blade flow matters as much as the cell itself. The blade has to arrive at the cell, be presented correctly and leave again without blocking other work, so the route from the finishing area to root machining and on to dispatch should be drawn before the cell position is fixed.
Acceptance and ramp-up
Agree before installation how the cell will be accepted. A clear test usually names the blade type, the measurements to be taken, who takes them and the tolerances that count as a pass. Measuring the first blades on the root face and bolt circle, and comparing the results with the hub interface drawing, gives both sides an objective reference.
The first weeks also set habits for the life of the cell. Operators should be trained on referencing and the manual hole check, maintenance staff on tool changes and the slurry system, and quality staff on reading the logged data. Plants that involve their own people during commissioning tend to reach steady output sooner, because the knowledge stays on site when the commissioning team leaves.
For manufacturers setting up or expanding blade capacity as part of a larger turbine program, the broader production picture is set out in the article on wind turbine manufacturing.
Who TurboMac Is For
TurboMac from Cybernetik
Cybernetik Technologies has been building industrial automation for more than three decades, with a team of over 600 professionals and more than 400 customized robotic solutions delivered. TurboMac belongs to its CleanTech division, which also works on EV and energy storage battery packs and catalytic converter production. The system is presented on the wind turbine blade machining solution page.
TurboMac is designed and built in India, at manufacturing units in Pune, Kheda in Gujarat and Raigad, with a design center in Pune and a North American office in Summerville, South Carolina. For Indian blade plants, that puts engineering and service close at hand.
What sets the system apart: