Key takeaways
A catalytic converter is mostly an empty honeycomb until it is coated. The washcoat, carrying the precious metals that do the chemistry, is a thin layer spread over thousands of tiny channels, and it decides whether the part meets its emission target. Put too little on and the converter underperforms. Put too much on and the plant gives away expensive metal and may block the channels it was meant to line.
Cybernetik automates catalytic converter coating as a complete line, from washcoat preparation through coating, drying, calcining and inline checks. Every part is barcoded and scanned, coated in two passes from opposite ends, dried in hot air at 150 to 200 °C, calcined at 600 to 650 °C, and verified through three-stage weight checking and a back pressure test, with robots handling the parts and accepting or rejecting them after the critical stages.
This article looks at how that automation is organized, what decisions it makes at each point, and what a manufacturer should plan for when setting up a coating line.
Why Coating Is the Step to Automate First
Most of the value in a finished catalyst sits in the coating. The substrate itself is a fixed, bought-in part. The washcoat and the precious metals in it are where the cost and the performance both live, so small variations at this step carry through to the price of every part and to whether the vehicle passes its emissions test.
Coating is also where manual work struggles most. Parts are fragile, especially after coating and before calcining. The coating has to be even along the full length of the part. Channels must stay open. And a manufacturer supplying vehicle makers under BS-VI rules in India, or equivalent standards elsewhere, needs records showing that each part was made correctly.
Those pressures are why Cybernetik treats coating as a system rather than a single machine. How the substrate itself is made and how ceramic and metallic types differ is covered in the guide to the catalytic converter substrate.
The Four Automation Groups
Cybernetik’s substrate coating system brings several automation systems together, which it groups into four areas. Each one controls a different source of variation.
| Automation group | Equipment | What it controls |
|---|---|---|
| Washcoat automation | Premix tanks, brewing tanks, activation tanks, portable tanks | A consistent blend reaching the coater, batch after batch |
| Coating automation | Coating machine, air stripper | How much washcoat each part takes up and whether the channels stay open |
| Substrate handling and thermal processing | Dryer, calciner, robotic pick and place, track and trace | Safe movement of fragile parts, correct heat treatment and a record of every part |
| Quality checks | Back pressure checking station, weighing station | Proof that each part carries the right coating and flows freely |
Looking at the line this way helps when diagnosing problems. Weight scatter can usually be traced to the blend or the coater. Damaged parts point to handling. Blocked channels sit between the air stripper and the back pressure check. When all four groups are designed together, the data from one can explain what shows up in another.
The Decisions the Line Makes
A coated substrate passes through 14 steps on Cybernetik’s line. Rather than walking through them one by one, it is more useful to look at the points where the automation actually decides something about the part.
| Point in the line | Decision the automation makes |
|---|---|
| Barcode printing and verification | Gives the part an identity and confirms it can be read before any value is added |
| Scanning before coating | Decides whether the part is due its first or second coating pass |
| After coating | Robot sends correctly coated parts on to drying and moves poorly coated parts to a reject conveyor |
| After first drying | Flip-over unit inverts the part so the second pass coats from the other end |
| After calcining | Robot places the part on the weigher so the final coating weight can be confirmed |
| Back pressure station | Checks for blocked channels before the part is released |
Identity before value
Parts are loaded onto a belt conveyor and given an identity straight away, using a barcode scanner, a laser printer and a pad printer. Marking the part before coating means every later result, from coating weight to back pressure, attaches to that one part. If a problem appears months later, the plant can look back at exactly how that part was made.
Knowing which pass comes next
Each part is scanned before coating to determine whether it is at the first or second coating stage. This is a small step with a large effect. In a two-pass process, a part coated twice from the same end, or sent to calcining after only one pass, looks almost the same as a good part. Letting the scanner decide removes that risk from the operator.
Coating and stripping
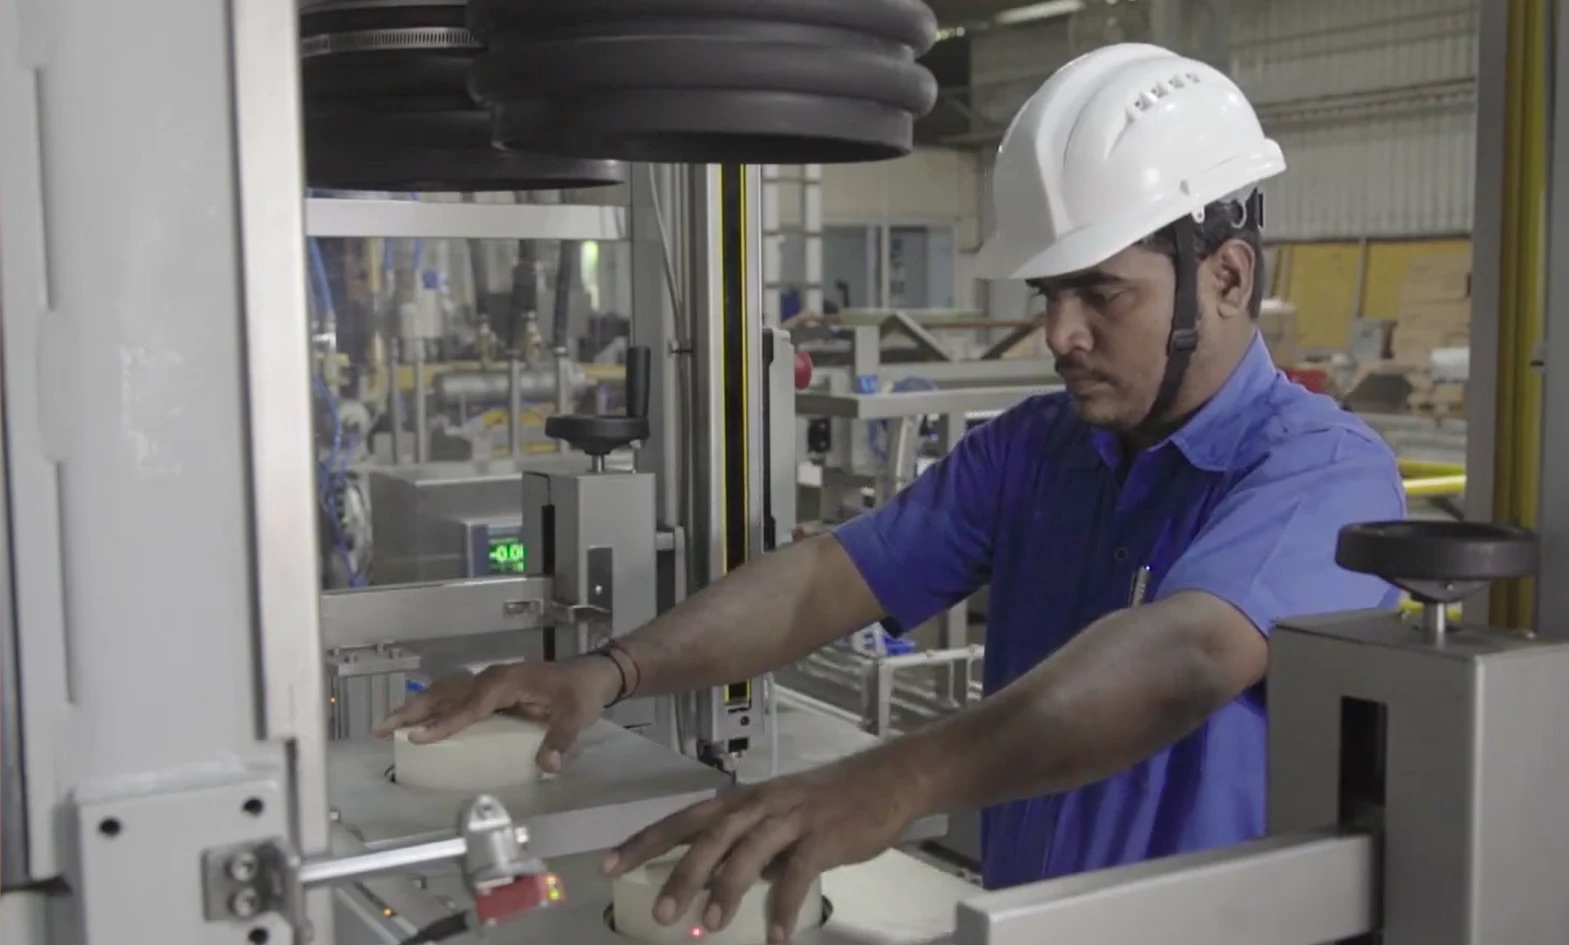
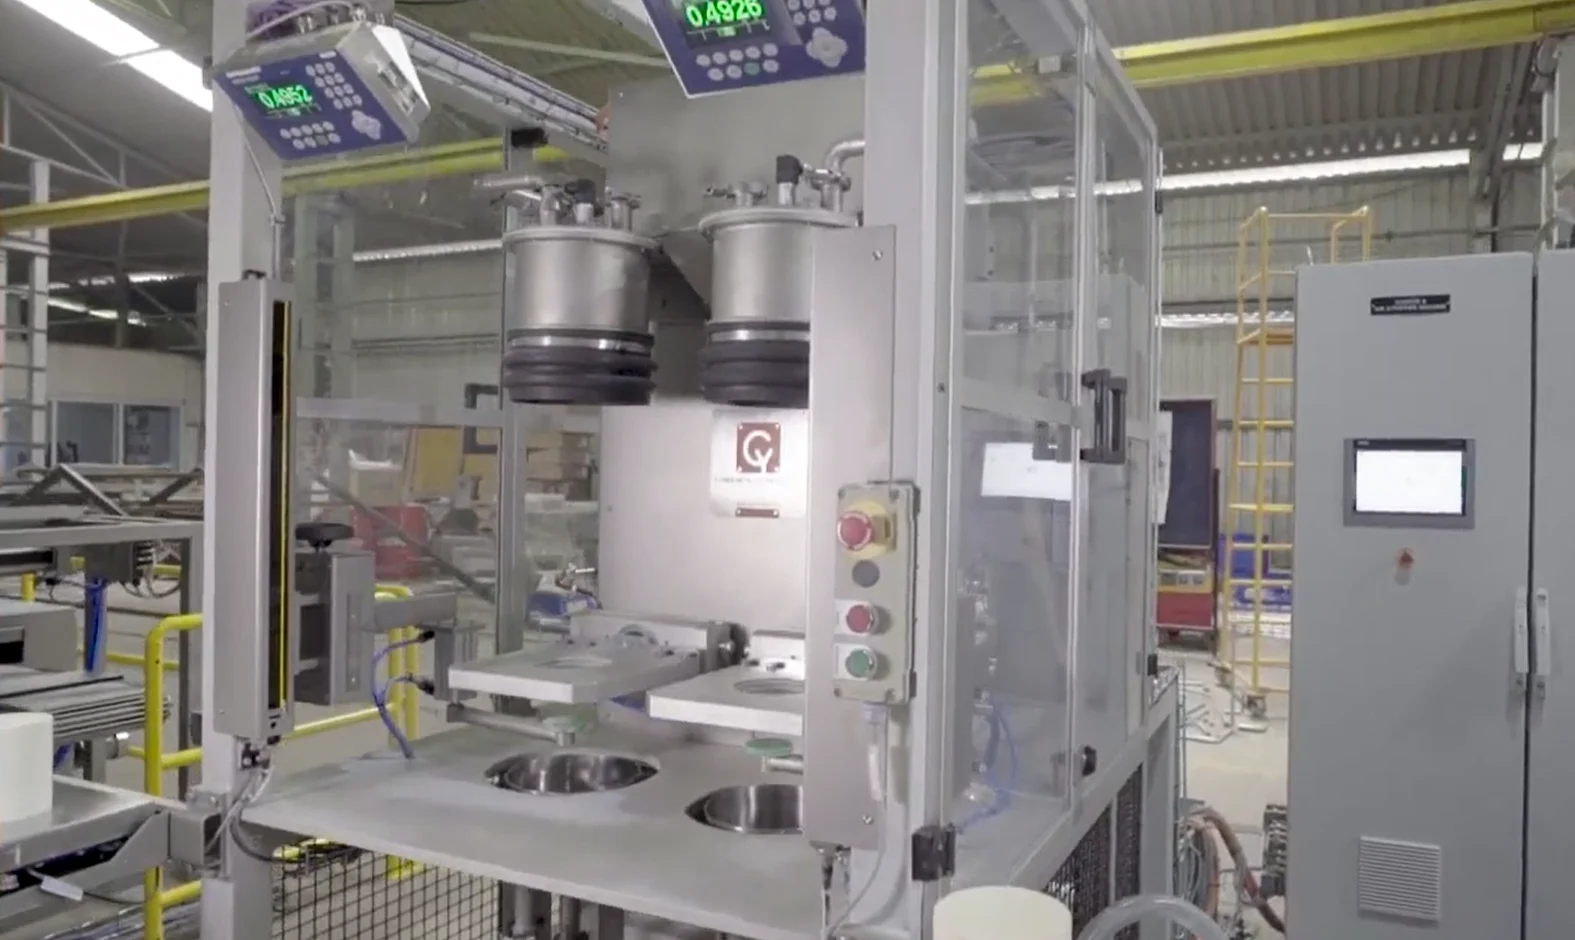
The coating machine rotates the part through 360 degrees in stages in the horizontal plane while washcoat is applied. An air stripper then clears excess slurry from the channels. Getting this balance right is what keeps coating weight on target without leaving blocked cells.
Accept or reject straight after coating
A robot on a servo slide moves correctly coated parts to a pallet, which a pusher slide feeds into the drying tunnel. Parts that are not properly coated go to a reject conveyor instead. Catching them here, before drying and calcining, saves the energy and time of heat treating a part that will be scrapped anyway.
Drying, flipping and the second pass
The drying tunnel uses hot air at 150 to 200 °C. Dried parts move along an accumulation conveyor to a flip-over unit, which turns them upside down. A robot returns the inverted part for its second pass, which runs through the same scan, coat and dry steps from the other end. Coating from both ends gives a more even profile along the part than a single pass can.
Calcining and final checks
After both passes, a robot removes the part and sends it to the calciner, which runs at 600 to 650 °C to fix the washcoat. A further robot places the calcined part on the weigher, and a back pressure station checks for blockage before the part is released.
What Three-Stage Weight Checking Tells You
Cybernetik lists three-stage weight checking as part of its quality assurance. Weighing a part at more than one point in the process is useful because the difference between readings shows how much coating was added and kept, rather than just the final weight of the part.
A single final weight can hide two errors that cancel each other out, such as a heavy substrate with a light coating. Comparing readings separates the substrate from the coating and helps show where in the line a deviation started, which is far more useful than knowing only that a part is out of limits.
Because coating weight relates directly to precious metal loading, these readings are also a cost control. Plants that track them closely tend to find steady savings in the metal they give away on parts that were coated slightly heavy.
Traceability That Means Something
Track and trace on Cybernetik’s line gives real-time access to process data for monitoring, control and later upgrades. In practice, that means a part number linked to its pass history, reject decisions, weights and back pressure result. That record is part of the wider shift toward connected process automation in manufacturing, where data from each station informs the next decision.
For a supplier to vehicle makers, this record does two jobs. It supports audits and customer queries, and it gives the plant the evidence it needs to find and fix the cause of a drift before it becomes a batch problem.
Line Configurations
Coating needs differ by vehicle type and substrate material. Cybernetik’s system is designed for heavy-duty trucks, passenger cars and motorcycles, and it has shown three configurations of its coating equipment.
| Configuration shown by Cybernetik | Where it fits |
|---|---|
| Passenger car standalone catalytic converter coating | Gasoline vehicle substrates, where a compact standalone setup suits the volume and part range |
| Substrate coating line for DOC, DPF and SCR catalysts | Diesel aftertreatment, where several catalyst types and larger parts move through one line |
| Rotary coater for metallic substrates with fixed volume doser and air stripper | Metallic foil substrates, often used in two-wheelers and compact applications |
The configuration follows from the product mix. A plant coating only passenger car parts has different needs from one serving diesel aftertreatment, and metallic substrates usually call for a different coater than ceramic ones.
 “Consistent coating weight is essential for catalyst performance and cost control. Three-stage weight checking helps monitor washcoat application, optimize precious metal loading, and detect process deviations early.”
See it in action
Manual Coating Versus an Integrated Line
Many plants start with manual or semi-automatic coating and add automation as volumes grow. The table shows where an integrated line changes the way the work is done.
| Manual or semi-automatic coating | Integrated automated line | |
|---|---|---|
| Part identity | Paper records or batch labels | Barcode printed, verified and scanned on every part |
| Which pass a part needs | Operator judgment and sorting | Scanner decides first or second stage automatically |
| Reject handling | Visual checks, often after the fact | Robot separates poorly coated parts straight after coating |
| Part handling | Manual lifting of fragile coated parts | Robotic pick and place between stations |
| Coating weight check | Sampling | Three-stage weight checking |
| Blockage check | Occasional or end of batch | Back pressure station on the line |
| Records | Scattered across shifts and stations | Track and trace data with real-time access |
Cybernetik also lists inbuilt systems for safe operation. Coating lines combine robots, heavy fragile parts and high-temperature equipment, so guarding and safe access are part of the design rather than something added afterward.
Running the Line Day to Day
Automation removes many manual decisions, but how a plant runs the line still shapes the results. A few habits make the difference between a line that holds its quality and one that drifts.
The data from track and trace makes these habits practical. Instead of relying on memory or shift notes, supervisors can see when a change started and which parts it affected, and act before a whole batch is at risk.
Planning a Coating Line
| Question to settle early | Why it matters |
|---|---|
| Which substrate types and sizes will the line run? | Ceramic and metallic parts, and gasoline and diesel catalysts, can need different coater types and handling |
| How many coating passes does each product need? | Pass count and drying capacity set the line rate as much as the coater does |
| Where will the line weigh parts, and what limits apply? | Weight limits tie directly to precious metal content and cost |
| How will reject parts be handled and reviewed? | A reject conveyor is only useful if someone acts on what it collects |
| What does the plant system need from the line? | Traceability data is worth more when it connects to quality and customer records |
| What utilities do the dryer and calciner need? | Heat treatment at 600 to 650 °C drives power and exhaust planning for the building |
These answers shape the layout, the number of robots and the size of the dryer and calciner. Settling them before equipment is chosen avoids a line that runs well on one product and struggles with the next.
Coating Automation from Cybernetik
Cybernetik Technologies has been building industrial automation for more than three decades, with a team of over 600 professionals and more than 400 customized robotic solutions delivered. It is headquartered in Pune, with two design offices and four manufacturing plants, and a North American office in Summerville, South Carolina. Its CleanTech division covers catalytic converter production alongside EV and energy storage battery packs and wind turbine blade machining.
The coating system is described on the catalytic converter substrate coating solution page, which sets out each step of the line.
What the coating system brings: