Key takeaways
The exhaust pipe on a modern diesel truck is doing more chemistry than most people realize. Between the turbocharger and the tailpipe sit a catalyst, a filter, an injector spraying a urea solution, a second catalyst and often a third, with sensors reading temperature, pressure and NOx throughout. None of it would exist if diesel engines could simply burn fuel cleanly.
Diesel aftertreatment is the sequence of devices that cleans diesel exhaust after combustion. A diesel oxidation catalyst removes carbon monoxide and hydrocarbons, a diesel particulate filter traps soot and periodically burns it off, and selective catalytic reduction uses ammonia from a urea solution to convert NOx into nitrogen and water. The devices depend on each other, which is why problems with one usually show up as symptoms in another.
Why Diesel Engines Need All This
A diesel engine burns fuel with far more air than it needs. That makes it efficient, and it creates two pollutants that are difficult to deal with together.
High combustion temperatures produce nitrogen oxides. Lowering those temperatures reduces NOx but leaves more unburned carbon, which means soot. Raising them burns the soot but makes more NOx. Engine designers have pushed this trade-off as far as it will go, and the limits in force today cannot be met by combustion control alone. The aftertreatment system exists to break that deadlock, by letting the engine run where it is efficient and cleaning the exhaust afterward.
The Devices in Order
| Position | Device | What it does |
|---|---|---|
| First | Diesel oxidation catalyst | Oxidizes carbon monoxide and hydrocarbons, and makes nitrogen dioxide for the devices behind it |
| Second | Diesel particulate filter | Traps soot, which is later burned off during regeneration |
| Third | Urea dosing unit | Sprays a urea solution into the hot exhaust, where it becomes ammonia |
| Fourth | SCR catalyst | Uses that ammonia to convert NOx into nitrogen and water |
| Last | Ammonia slip catalyst | Oxidizes ammonia that passes through unused |
The order is not arbitrary. The oxidation catalyst goes first because it is the simplest to light off and because the nitrogen dioxide it produces is useful downstream. The filter comes next so that soot does not foul the SCR catalyst. Urea is injected after the filter, where the exhaust is hot and relatively clean, and the ammonia slip catalyst sits last to catch anything unused.
The Diesel Oxidation Catalyst
This is a honeycomb brick with a washcoat carrying platinum and palladium. It oxidizes carbon monoxide and hydrocarbons into carbon dioxide and water, and it deals with the oily portion of particulate that condenses on soot.
Its more important job is making nitrogen dioxide. Converting part of the nitric oxide in the exhaust gives the filter a way to burn soot at lower temperatures than oxygen alone allows, and it improves the reaction in the SCR catalyst further along. A weak or aged oxidation catalyst therefore affects the whole system, not just its own numbers.
Like all catalysts, it does nothing below its light-off temperature, and diesel exhaust is cooler than gasoline exhaust. Cold starts and prolonged idling are where most untreated emissions occur.
The Diesel Particulate Filter
The filter is also a honeycomb, but with alternate channels plugged at opposite ends. Exhaust has no straight path through, so it is forced through the porous walls, and soot is left behind on the channel surfaces. Modern filters remove the large majority of particulate mass and are even more effective on the small particle counts that current standards target.
Trapping soot is the easy part. Getting rid of it is where the engineering sits, because a filter that keeps filling up eventually blocks.
Regeneration: Burning the Soot Away
| Type | How it happens | When it is used |
|---|---|---|
| Passive | Soot burns continuously using nitrogen dioxide at normal exhaust temperature | Steady highway running at reasonable load |
| Active | The engine raises exhaust temperature deliberately to burn soot off | When filter loading rises and passive burning is not enough |
| Parked or forced | A technician triggers regeneration with the vehicle stationary | When the filter is heavily loaded and normal regeneration has failed |
Passive regeneration is the quiet, efficient version. On a vehicle running at steady load, exhaust is hot enough and the nitrogen dioxide from the oxidation catalyst burns soot continuously, so the driver notices nothing.
Active regeneration happens when that is not enough. The control system raises exhaust temperature, usually by injecting extra fuel that burns over the oxidation catalyst, until the soot ignites. It costs fuel and takes several minutes, and it needs the vehicle to keep running while it completes.
This is where city vehicles struggle. Short trips, heavy traffic and long idling keep exhaust temperatures low, regenerations are started and interrupted repeatedly, and soot accumulates faster than it is removed. Many filter problems on urban delivery vehicles, buses and vans trace back to duty cycle rather than to any fault in the hardware.
Ash Is Not Soot
Soot burns. Ash does not. Ash comes mainly from metallic additives in engine oil, and it collects in the filter permanently, slowly reducing the space available for soot.
That means every filter eventually needs cleaning or replacement regardless of how well regeneration works, usually at high mileage. Two practical consequences follow for fleets. Oil consumption directly affects filter life, so an engine burning oil shortens the interval. And using the oil specification the manufacturer requires matters, because low-ash oils were developed specifically to slow this process.
Selective Catalytic Reduction
SCR is what finally deals with NOx. A metered amount of urea solution is sprayed into the hot exhaust, where it decomposes into ammonia, and the ammonia reacts with NOx over the SCR catalyst to produce nitrogen and water, both harmless.
Done well, it removes a large majority of the NOx, which is why it became the standard route for heavy diesel engines. The catalyst itself is usually based on copper or iron zeolites, and the SCR brick is often combined with the particulate filter in one unit on newer vehicles to save space and help it reach temperature faster.
Why temperature matters so much
Urea does not decompose cleanly below roughly 180 to 200 degrees Celsius. Inject it into exhaust that is too cool and instead of ammonia you get solid deposits in the pipe and on the injector, which block the spray and reduce conversion. Control systems therefore hold off dosing until the exhaust is warm enough, which is another reason low-load city operation is harder on these systems than highway running.
Ammonia storage
The catalyst stores a quantity of ammonia on its surface, which lets it keep converting NOx through brief changes in engine load. The control system tracks how much is stored and doses accordingly. Too little and conversion drops; too much and ammonia escapes from the tailpipe, which is what the ammonia slip catalyst at the end is there to prevent.
 “Every stage of diesel aftertreatment contributes to emissions performance. From oxidation and soot filtration to NOx reduction, component quality and system integration determine long-term reliability.”
See it in action
The Urea Solution
The fluid is a solution of around 32.5 percent urea in demineralized water, sold under names such as AdBlue or diesel exhaust fluid. The concentration is not arbitrary; it is the mixture with the lowest freezing point, which matters in cold regions where tanks and lines are heated for winter operation.
Quality and handling cause more trouble than the chemistry. The solution has a limited shelf life and degrades faster in heat, which is relevant across much of India. It must not be contaminated, since diesel, dust or ordinary water will damage the dosing system or the catalyst. And topping up from open containers in a dusty yard is a common route for contamination. Fleets that treat it as carefully as they treat fuel have noticeably fewer SCR problems than those that do not.
Exhaust Gas Recirculation
EGR sits on the engine rather than in the exhaust system, but it belongs in the picture. Routing some exhaust back into the intake lowers peak combustion temperature and cuts NOx formation at source.
The trade-off is familiar: less NOx, more soot. How much work is given to EGR versus SCR is a design choice. Leaning on EGR means more soot and more demand on the filter; leaning on SCR means more urea consumption. Most modern heavy engines favor SCR, which allows combustion to be tuned for efficiency and lets the aftertreatment handle NOx.
Sensors and Control
None of this works without measurement. A typical system carries temperature sensors at several points, a differential pressure sensor across the filter to estimate soot loading, and NOx sensors before and after the SCR catalyst to check conversion and guide dosing.
Onboard diagnostics watch all of it. If conversion falls short, if the filter will not regenerate or if the urea tank runs empty, the system warns the driver and then restricts engine power. That behavior is deliberate and required, and it is why a sensor fault can leave a vehicle derated even though the engine itself is healthy.
The Indian Picture
India moved from BS IV straight to BS VI in April 2020, which introduced these systems across the market in one step rather than gradually. Real driving emissions testing added afterward means the system has to perform in ordinary traffic rather than only on a test cycle, which puts weight on exactly the low-speed, low-temperature conditions that are hardest for aftertreatment.
For operators, three practical issues follow. Urea availability and quality vary outside major routes. Duty cycles in Indian cities involve long idling and slow traffic, which works against both regeneration and SCR dosing temperatures. And tampering, usually to avoid urea cost or clear a warning, remains a problem that damages the rest of the system and leaves the vehicle non-compliant.
What Goes Wrong
| Problem | What causes it | What it leads to |
|---|---|---|
| Filter blocking | Short trips and idling that never let regeneration complete | Rising backpressure, warning lamps, loss of power |
| Ash build-up | Engine oil consumption over long service life | Filter cleaning or replacement at high mileage |
| Poor urea quality | Contaminated, diluted or expired solution | Crystal deposits, blocked dosing, reduced NOx conversion |
| Deposits in the dosing area | Urea injected below the temperature it needs | Blocked injector and uneven spray |
| Sensor faults | NOx, temperature or pressure sensors drifting or failing | Wrong dosing, unnecessary regeneration, derated engine |
| Tampering | Removing or disabling devices to avoid running costs | High emissions, legal exposure, damage to the rest of the system |
A pattern runs through that table. Most aftertreatment failures are not component defects. They come from duty cycle, fluid quality or engine condition, and the aftertreatment is simply where the symptom appears.
Keeping a Fleet Running
Making These Components
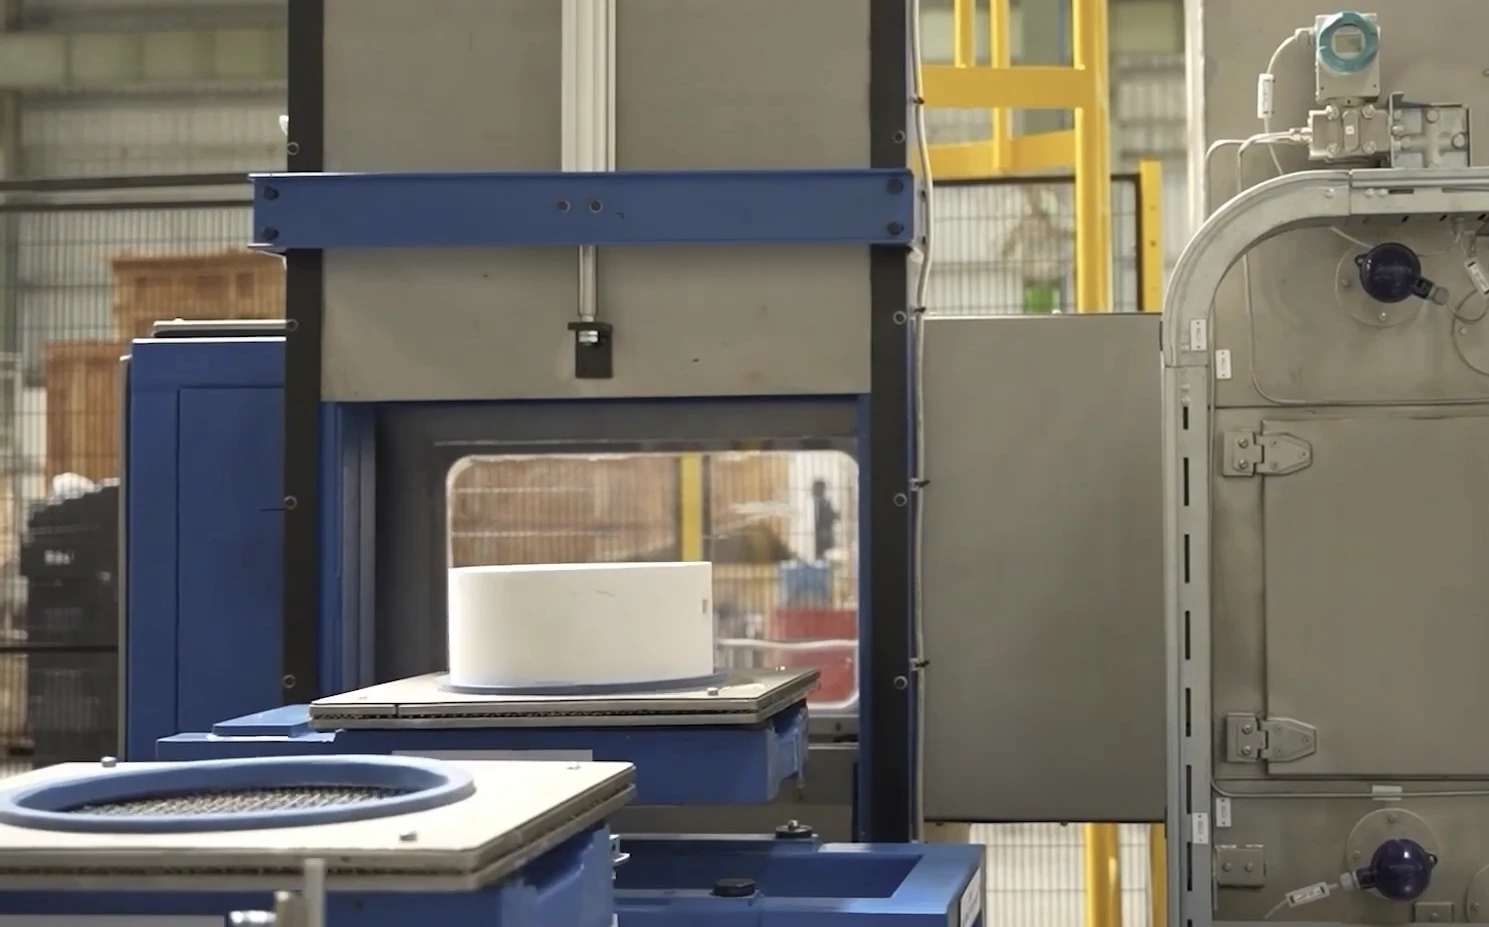
From a manufacturing standpoint, the three main devices share a production logic. Each starts as a fragile ceramic honeycomb, receives a coating whose uniformity determines performance, goes through a controlled thermal cycle, and is then wrapped and pressed into a steel can with enough force to hold it through years of vibration without cracking it.
Coating uniformity is the recurring challenge, and it matters for cost as much as for emissions, since the precious metals involved are the dominant material expense. The substrate itself, its channel structure and how coating behaves inside it are covered in the article on catalytic converter substrates.
Filters add their own requirements, including plugging alternate channels accurately and verifying that the walls filter as designed, while SCR units bring dosing hardware and mixing sections that have to be assembled and leak tested. Across all of them, traceability matters, because an emissions component may be questioned years after it was built.
Automation from Cybernetik
Cybernetik builds automation for emission control component manufacturing as part of its CleanTech work, where the demands are precise handling, repeatable process control and records that last rather than raw speed.
Those demands come from the parts themselves. Thin-walled ceramic substrates chip and crack, and by the time one carries a coating it represents real material value, so how it moves between stations shows up directly in scrap. Coating consistency decides both performance and precious metal cost. And because the finished unit is an emissions component, the data tying each one to its process parameters has to survive long after it leaves the plant. The wider range of work is set out under CleanTech automation.
Cybernetik has delivered more than 400 custom robotic automation solutions and over 6,000 systems across 30 plus countries, covering handling, process control, inspection and traceability in automotive and CleanTech manufacturing. Systems are engineered for the specific component rather than adapted from a standard model, and projects run from design through factory acceptance testing, installation and commissioning with one team responsible throughout.