Key takeaways
A battery pack in an electric car sits bolted into the floor, cooled by liquid, sheltered from the weather and rarely touched for years. A pack in an Indian electric scooter gets pulled out and carried up stairs to charge, splashed through flooded roads during the monsoon, baked in summer heat and shaken over broken surfaces every day.
The scooter pack is smaller and simpler on paper. In practice it lives a harder life, and the assembly line has to build for that life rather than for the specification sheet.
India’s electric vehicle volume sits overwhelmingly in two and three wheelers rather than cars, a pattern covered in the article on EV battery production trends in India. This piece looks at what that means for how these packs are actually built.
Smaller Packs, Different Problems
| Electric scooter or motorcycle | E-rickshaw | Passenger car, for contrast | |
|---|---|---|---|
| Typical system voltage | Commonly 48 to 72 volts | Commonly around 48 to 60 volts | Several hundred volts |
| Pack energy | A few kilowatt-hours | Larger than a scooter, far smaller than a car | Tens of kilowatt-hours |
| Common cell choice | Cylindrical, in high counts | LFP prismatic or cylindrical, chosen for cycle life | Varies widely by platform |
| Cooling | Usually passive or air | Usually passive | Often active liquid cooling |
| Handling in service | Often removed for charging or swapped | Increasingly swapped at stations | Fixed in the vehicle floor |
| Hardest conditions | Water, dust, vibration, heat, drops | Long daily duty, heavy loads, deep cycling | Crash loads and structural duty |
The last row of that table is the one that shapes assembly most. A car pack is engineered around crash safety and structural duty. A scooter pack is engineered around being handled, dropped, soaked and shaken, and an e-rickshaw pack around being worked hard for long hours every single day. Those are different failure modes, and they call for different emphasis on the line.
Voltage Changes What the Line Needs
Most two and three wheeler packs run at far lower voltages than car packs, commonly somewhere between 48 and 72 volts. That changes the electrical safety picture on the line compared with a car plant handling packs at several hundred volts.
It does not remove it. A fully charged pack at these voltages can still deliver very high current into a short circuit, enough to weld a spanner in place or start a fire, and the upper end of that range sits above the level usually treated as safe to touch. The difference is one of degree. Insulated tooling, a defined order for making connections and a clear response to a damaged pack all still apply.
Cylindrical Cells Mean a Lot of Joints
Many two-wheeler packs use cylindrical cells, and because each cell holds relatively little energy, a pack needs a large number of them. More cells means more joints. A pack that looks modest from the outside can contain hundreds of welds, each one carrying current and each one exposed to vibration for years.
That shifts the weight of quality control toward joining. The choice between resistance welding, laser welding and wire bonding, and how each is checked, is covered in the guide to laser welding and wire bonding for cell interconnects. Whichever method is used, a joint count in the hundreds is exactly the situation where sampling stops being meaningful and every joint needs checking.
Built to Be Carried
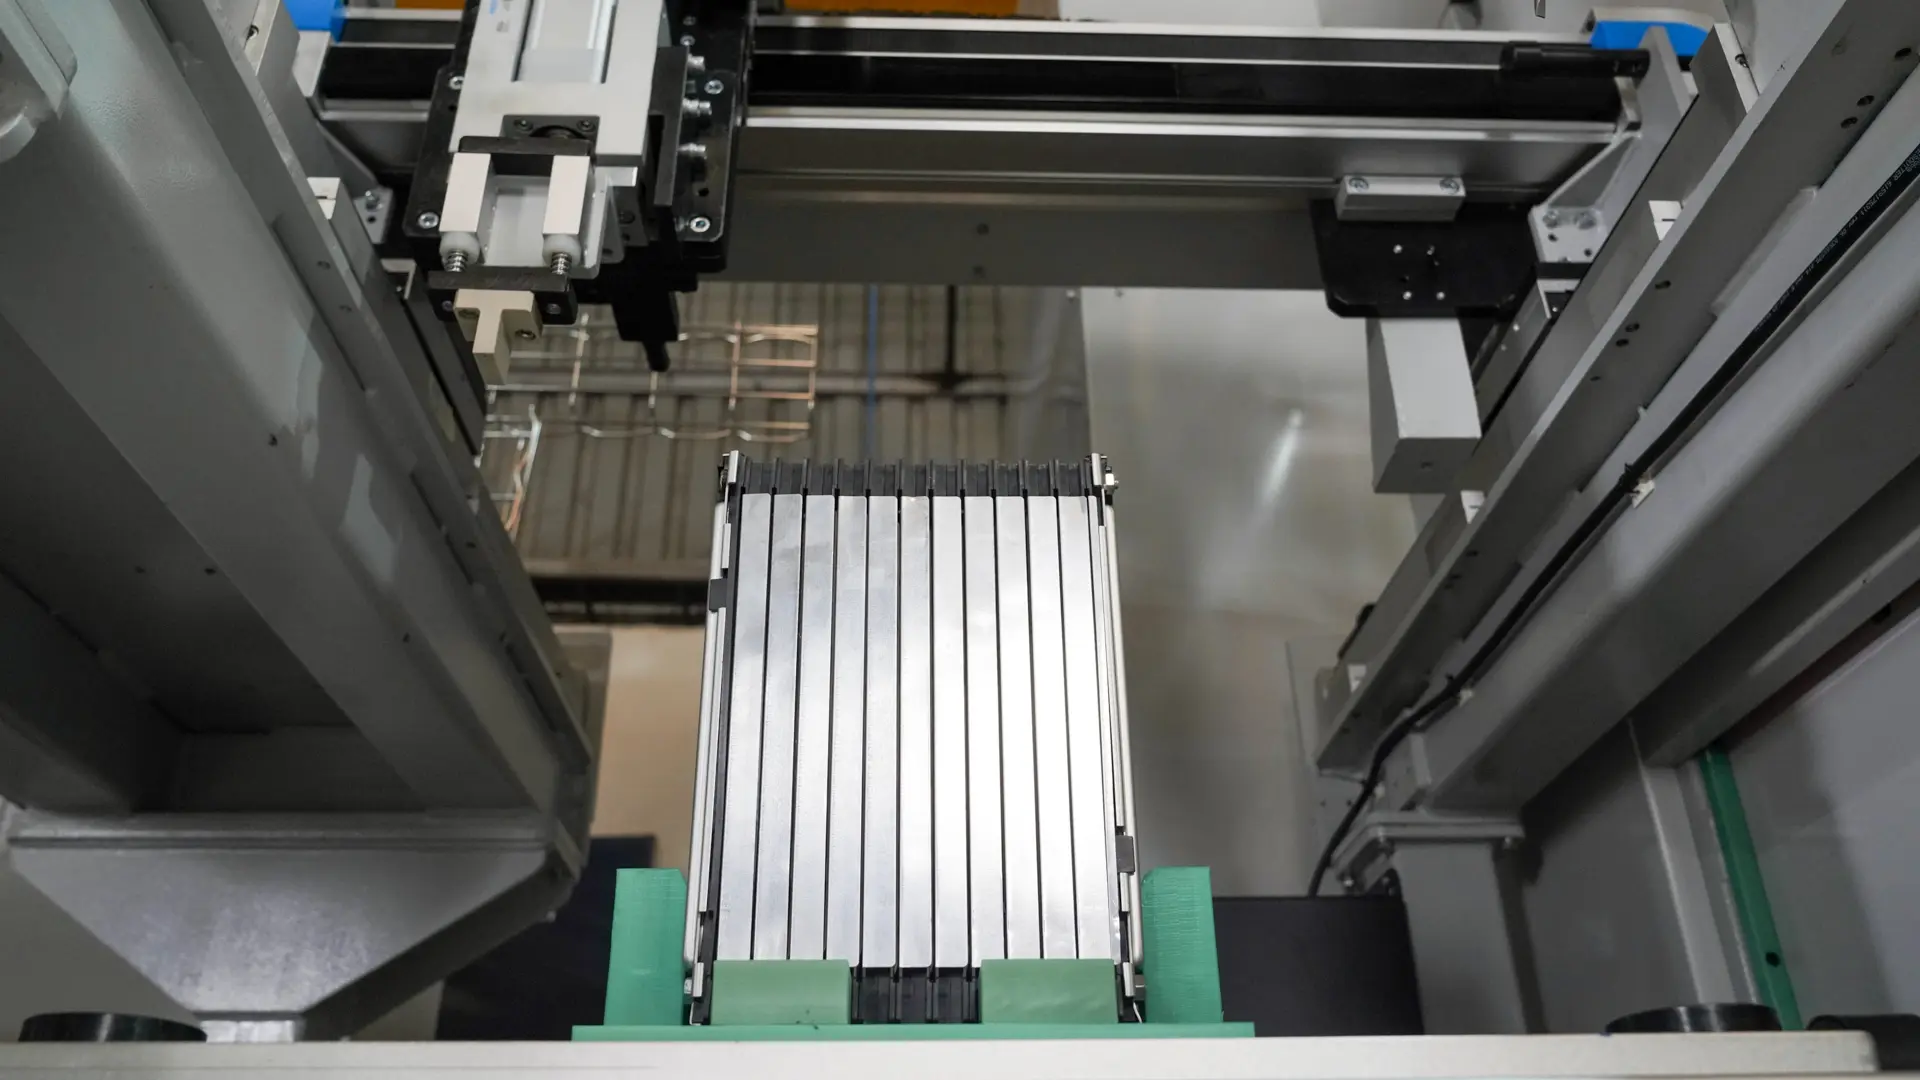
Removable packs are common on Indian scooters because many owners do not have a charging point where they park. A pack that gets lifted out and carried around faces demands a fixed pack never sees.
Connectors
The connector between pack and vehicle may be mated and unmated every day for years. A connector rated for a modest number of cycles, or one that allows dirt into the contact area, becomes a source of heating and intermittent faults long before the cells wear out.
Drops and knocks
A pack that gets carried will eventually get dropped. Enclosure strength, how cells are held inside and how well the internal structure absorbs a shock all decide whether a drop is harmless or starts a slow internal fault.
Enclosure robustness
A casing that is scuffed, knocked and set down on rough floors every day needs more margin than one that sits untouched under a car. Seals and fasteners have to survive that treatment and still keep water out.
Monsoon and Dust
Water is the enemy of any battery pack, and Indian roads during the monsoon test that thoroughly. A scooter pack sits low, close to spray and standing water, and waterlogged streets can submerge it briefly.
That makes sealing one of the most important things the line gets right, and leak testing one of the most important checks. How that testing works, and why temperature affects the result so strongly, is covered in the article on leak testing methods for battery enclosures.
Dust matters too, especially for anything with vents, connectors or gaps. Fine dust mixed with moisture forms a conductive paste over time, which is a slower route to the same kind of failure water causes quickly.
Heat Without Liquid Cooling
Most two and three wheeler packs rely on passive or air cooling rather than liquid systems. Add high ambient temperatures across much of India and the thermal margin gets thin.
Without a liquid system to even out temperatures, the pack depends on its internal layout, the materials between cells and the enclosure, and above all on the cells being well matched. A cell that runs a little warmer than its neighbors ages faster, which makes it warmer still, and in a pack with no active cooling to pull that difference back there is nothing to stop the gap widening.
The practical result is that cell grading and thermal layer placement matter more in these packs, not less, even though the packs are smaller and cheaper.
Vibration and Road Conditions
Scooters and rickshaws transmit far more road vibration to their batteries than cars do, and many roads add potholes and speed breakers on top. That vibration works on every joint, bracket and cable inside the pack continuously.
A weld that is slightly weak will usually pass every test on the day it is made. Months of vibration are what find it. The same goes for a cable routed against a sharp edge or a cell held a little loosely. These are assembly details, and in this segment they decide whether a pack lasts its expected life.
E-Rickshaws Are a Different Duty
E-rickshaws deserve separate treatment because their use pattern is unlike a private scooter’s.
A private scooter is ridden for short trips and parked most of the day. An e-rickshaw often runs for long hours with heavy passenger loads and gets drained deeply before charging, day after day. That is a demanding cycle, and it is a big part of why lithium iron phosphate has gained ground in this segment, since it tolerates repeated deep cycling well and stays thermally stable.
The segment has also been moving away from lead-acid batteries toward lithium, which changes what operators expect. A lithium pack costs more upfront and is expected to last much longer, so a pack that fails early does far more damage to trust than a cheap lead-acid battery ever did.
Battery Swapping Raises the Stakes on Identity
Swapping is growing fastest in exactly these segments, particularly for commercial fleets. A rider pulls into a station, hands over a depleted pack and leaves with a charged one in a couple of minutes.
That model changes the life of a pack completely. Instead of living in one vehicle, a swappable pack passes through dozens or hundreds of them, each with a different rider and duty. Tracking its health, its history and any fault it has shown becomes essential, because the operator needs to know which packs are aging faster and why.
All of that depends on every pack carrying a reliable identity from the day it was built, with its build record attached. How that works on the line is covered in the article on battery pack traceability and MES integration.
Swapping also pushes toward standard pack sizes and connectors so that one station can serve many vehicles. For manufacturers that means building to tight dimensional tolerances, because a pack that does not fit the slot is useless regardless of its cells.
 “As battery swapping expands, pack identity and traceability become essential for tracking health, service history, and performance across multiple vehicles.”
See it in action
Line Design for This Segment
Two and three wheeler pack lines tend to share a few characteristics that set them apart from car pack lines.
Pack counts are high and cell counts per pack are lower, so takt times are short and the pack assembly stages often set the pace rather than cell handling. Variant mix is usually wide, with several voltages and capacities built on the same line, which makes quick changeover valuable. And cost pressure is severe, which argues for automating the steps where consistency matters most, such as cell testing, joining and leak testing, while keeping simpler steps manual where that makes sense.
What should not be traded away for cost is verification. In a segment where packs take this much punishment, the defects that matter most are the ones that pass on the day and fail in the field, and those are only caught by checking every cell and every joint as the pack is built.
Compliance
India’s safety framework for these vehicles tightened considerably after the two-wheeler battery fires of 2022. AIS-156 covers electric power train safety, IS 16893 covers lithium-ion cells and IS 17387 covers battery packs. Together they push manufacturers toward documented testing and records for each pack, which is another reason traceability belongs in the line from the start.
Cybernetik’s Work in This Segment
Much of Cybernetik’s battery work has been for exactly this market, with battery pack assembly automation delivered for manufacturers including Hero MotoCorp, TVS Motor, Livguard and Matter.
| Cybernetik pack assembly capability | Specification |
|---|---|
| Cell formats | Cylindrical 18650, 21700 and 32140, plus prismatic, pouch and blade |
| Cell diameters | 32, 33, 35, 40, 42 and 46 mm |
| Line rate | Up to 6,000 cells per hour |
| Incoming verification | OCV, IR and ACIR testing on every cell with robotic sorting |
| Joining | Laser and resistance welding with inline weld integrity testing on both module faces |
| Placement checks | Insulation detection and polarity checking on every unit |
| Pack assembly | Thermal pads and insulation sheets, BMS mounting, gasket and cover assembly |
| End of line | BMS and TCU programming, air leakage testing, electrical testing and laser marking |
| Module flexibility | Assembly lines adaptable to multiple module configurations |
| Traceability | Barcode and RFID capture with MES connectivity and process logging |
Three parts of that specification line up directly with the points above. Weld integrity testing on both module faces addresses the high joint counts and the vibration that finds weak welds. Air leakage testing on every pack addresses monsoon water. And lines adaptable to multiple module configurations suit a segment where several voltages and capacities often share one line.
Cybernetik has been building automation for more than three decades. It is headquartered in Pune with facilities in Gujarat and Raigad and offices in the United States and UAE, and has installed over 6,000 systems in more than 30 countries, including over 400 custom robotic solutions. More background is on the Cybernetik about page.