Key takeaways
For years sodium-ion sat in the category of promising chemistry that never quite arrived. That changed in the last eighteen months. CATL launched its Naxtra sodium-ion brand in April 2025 and said large-scale cell production had begun, and a passenger car built around sodium-ion cells has since been unveiled for a mid-2026 market launch.
So the question for manufacturers has shifted. It is no longer whether sodium-ion will reach production. It is what has to change on a line to build it, and how much of an existing lithium setup carries over.
The short answer is that more carries over than people expect, and the parts that do change are specific and worth understanding. This piece goes through both.
Why Sodium-Ion Is Getting Attention Now
The appeal starts with materials. Sodium is abundant and widely available, and sodium-ion cells need no lithium, cobalt or nickel. For any country or company worried about supply of those materials, that alone makes the chemistry worth watching.
Performance in the cold is the other big draw. CATL describes its sodium-ion cells as operating from minus 40 to 70 degrees Celsius, and reports strong capacity retention at very low temperatures, which is exactly where lithium chemistries struggle.
The trade-off is energy density. CATL reports around 175 Wh/kg for its current sodium-ion cells and says it aims to reach parity with lithium iron phosphate within a few years. For now, sodium-ion packs are generally larger or heavier than lithium packs holding the same energy, which is why early use has concentrated where that matters less.
The Headline: Much of the Line Carries Over
Sodium-ion cells are built using broadly the same steps as lithium-ion cells. Electrodes are coated, dried, calendered and slit. Cells are wound or stacked, filled with electrolyte, sealed and formed. Packs are assembled from cells using the same kinds of handling, joining, sealing and testing.
That familiarity is a large part of why the chemistry has been able to move quickly once the materials matured. A plant does not need to invent a new manufacturing discipline to make sodium-ion cells. It needs to adapt an existing one in a handful of important places.
Those places are where the rest of this article focuses.
What Changes at Cell Level
| Area | What changes with sodium-ion | What it means for manufacturing |
|---|---|---|
| Anode current collector | Aluminum on both electrodes instead of copper on the anode | Lower material cost and weight, and a very different tolerance of deep discharge |
| Anode material | Hard carbon rather than graphite | A less mature material that is harder to produce consistently at volume |
| Cathode material | Layered oxides, Prussian blue analogues or polyanionic compounds | Some are sensitive to moisture and air, which pushes up environmental control |
| Formation | Different first-cycle behavior from lithium chemistries | Protocols have to be developed for the chemistry rather than copied |
| Cell voltage | Generally a little lower per cell, with a more sloping curve | Different series counts for the same pack voltage, and re-set test limits |
| Energy density | Lower than lithium chemistries for now | Larger or heavier packs for the same energy, which suits some uses better than others |
Aluminum on both sides
In a lithium-ion cell the anode current collector is copper, because lithium reacts with aluminum at the anode potential. Sodium does not, so sodium-ion cells can use aluminum on both electrodes. Aluminum is cheaper and lighter than copper, which helps cost and weight directly.
It also changes how the cell tolerates being fully discharged. In a lithium-ion cell, taking the voltage too low can start dissolving the copper collector, which damages the cell. With aluminum on both sides that failure route largely disappears, which is why sodium-ion cells can typically be stored and shipped at a much lower state of charge than lithium cells. That has real consequences for handling and logistics, covered further down.
Hard carbon anodes
Graphite, the standard lithium-ion anode, does not store sodium well. Sodium-ion cells use hard carbon instead, and that material is less mature. Industry reporting on the chemistry has pointed out that hard carbon production is difficult to control at volume, and inconsistency in the anode material shows up directly in cell performance and yield.
Moisture and air sensitivity
Some sodium-ion cathode materials react with moisture or air, and that sensitivity has been flagged as a source of yield problems at scale. In practice it means tighter environmental control in electrode handling and cell assembly, similar in spirit to the dry-room discipline lithium cell plants already live with, but tuned to the particular materials in use.
Anyone who has run a lithium cell plant will recognize the pattern. The environmental and yield questions around sodium-ion are variations on the ones covered in the guide to battery cell manufacturing, applied to a different set of materials.
Formation
The first charge and discharge cycles set up the internal layers that decide how a cell ages, and sodium-ion cells behave differently in those cycles from lithium cells. Formation protocols therefore have to be developed for the chemistry rather than borrowed from an existing lithium process. This is one of the quieter areas where a plant converting to sodium-ion needs to invest learning time.
What Changes at Pack Level
For pack assembly the changes are smaller, but they are real and they are easy to overlook if a line is treated as simply swapping one cell for another.
Cell voltage and series count
Sodium-ion cells generally run at a slightly lower nominal voltage than lithium cells. To reach the same pack voltage, a pack needs more cells in series. That changes module layouts, busbar arrangements and the number of joints, even when the pack looks similar from the outside.
A different voltage curve
Sodium-ion cells tend to have a more sloping voltage curve than lithium iron phosphate, whose curve is notably flat through much of its range. That has a useful side effect. With a sloping curve, voltage tells you more about state of charge, which helps both battery management and any grading done on voltage.
The flip side is that every voltage-based limit on the line has to be set again for the new chemistry. Acceptance bands, sorting thresholds and state of charge checks built for a lithium cell are simply wrong for a sodium cell. How those measurements work in the first place is covered in the article on OCV, IR and ACIR testing.
Battery management settings
The BMS needs algorithms and limits written for the chemistry: voltage windows, state of charge estimation and protection thresholds. On a line that builds both lithium and sodium packs, loading the correct configuration for each becomes an important check, because the hardware can look identical while the settings are completely different.
Size and weight
Lower energy density means a sodium-ion pack holding the same energy is usually larger or heavier. That affects enclosures, mounting and handling on the line. It also shapes which applications suit the chemistry first.
Shipping and Storage Get Easier
The ability to hold sodium-ion cells at a very low state of charge is more than a technical footnote. It changes how cells can be moved and stored.
Lithium cells are shipped at a controlled partial charge, and they carry stored energy the whole way. Sodium-ion cells that can sit at a much lower charge carry far less stored energy in transit and in the warehouse, which reduces handling risk. For a pack plant, that has knock-on effects on how cells are received, how long they can sit, and what incoming checks need to confirm before they enter the line.
It also means incoming inspection has to recognize the difference. A voltage that would flag a lithium cell as dangerously discharged may be perfectly normal for a sodium cell shipped that way on purpose.
What Does Not Change
It is worth being clear about how much stays the same, because it is a large part of why sodium-ion adoption can move quickly.
CATL has also said its sodium-ion packs are designed to fit standard module formats, including battery swap formats, without significant design changes for vehicle makers. Wherever that holds, the pack-level change for an assembler is smaller still.
 “The future of flexible battery manufacturing lies in lines that can handle different cell formats, chemistry-specific limits, and BMS configurations without compromising traceability or production control.“
See it in action
Where Sodium-Ion Fits First
Analysts following the chemistry describe current use as concentrated in energy storage, low-range vehicles and auxiliary systems, with expansion into passenger and commercial vehicles underway. That pattern follows directly from the trade-offs.
That last group matters for India, where volume sits in cost-sensitive two and three wheelers and energy storage rather than long-range cars. The specific demands of those packs are covered in the piece on two-wheeler and e-rickshaw battery pack assembly. With no reliance on imported lithium, sodium-ion is a natural candidate to watch in those segments.
Living With Two Chemistries
CATL has described sodium-ion and lithium-ion as developing in parallel rather than one replacing the other. For manufacturers that probably means lines that have to handle both, sometimes on the same floor.
That puts a premium on flexibility. Lines that can take different cell formats, switch test limits and BMS settings by recipe, and keep the records of each chemistry separate will adapt to sodium-ion without major rebuilding. Lines built rigidly around one lithium cell will not.
The practical risk on a mixed line is the wrong settings meeting the right hardware: a sodium cell tested against lithium limits, or a sodium pack loaded with a lithium BMS configuration. Recipe control and identity tracking are what prevent that.
Building Lines That Are Ready for It
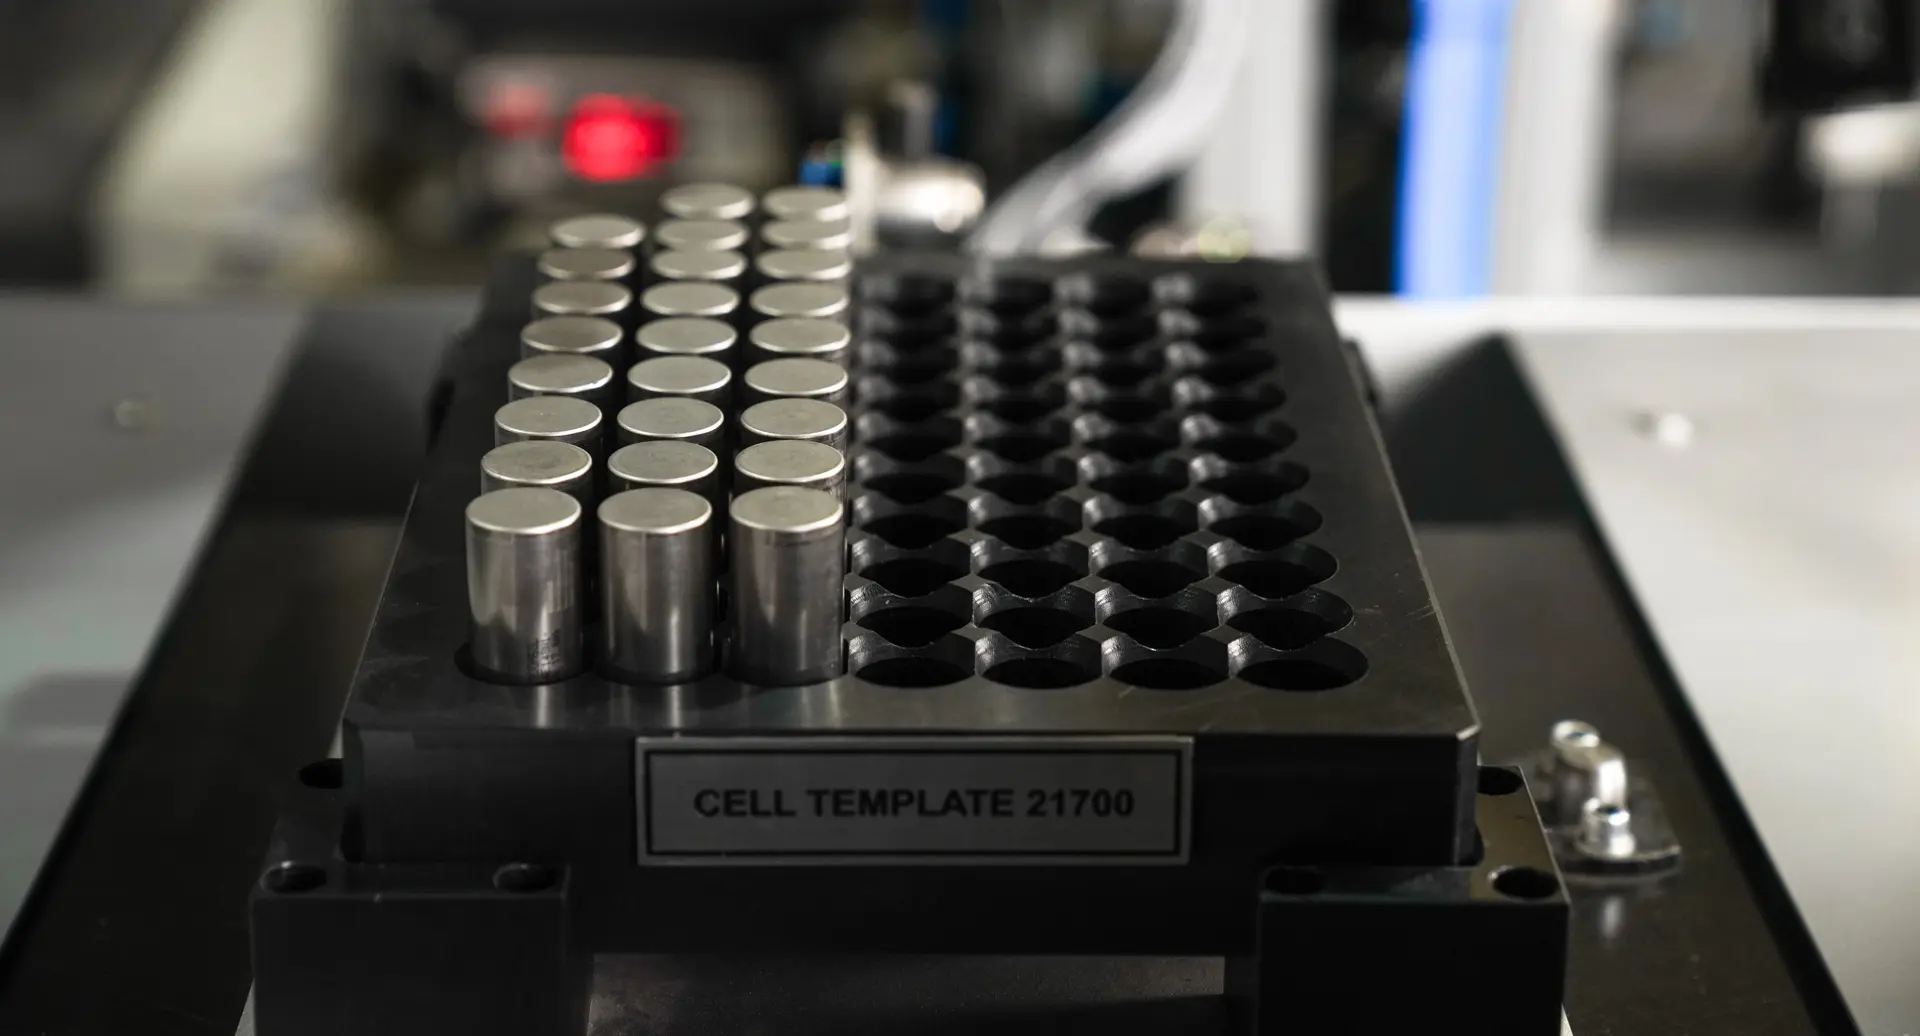
Cybernetik builds battery pack assembly automation rather than cell manufacturing equipment, so its work sits at the pack stage, which is where sodium-ion changes are smallest and flexibility matters most.
| Cybernetik pack assembly capability | Specification |
|---|---|
| Cell formats | Cylindrical 18650, 21700 and 32140, plus prismatic, pouch and blade |
| Cell diameters | 32, 33, 35, 40, 42 and 46 mm |
| Module flexibility | Assembly lines adaptable to multiple module configurations |
| Incoming verification | OCV, IR and ACIR testing on every cell with robotic sorting |
| Joining | Laser and resistance welding with inline weld integrity testing on every joint |
| End of line | BMS and TCU programming, air leakage testing, electrical testing and laser marking |
| Control | Unified PLC and SCADA with recipe-based operation |
| Traceability | Barcode and RFID capture with MES connectivity and process logging |
| Line rate | Up to 6,000 cells per hour |
The parts of that specification that matter for sodium-ion are the flexible ones. Handling a wide range of cell formats and multiple module configurations lets a line take on new cells without retooling from scratch. Recipe-based control means voltage limits, sorting thresholds and BMS settings can be changed for the chemistry in use. And cell-level testing on every unit means a new chemistry is checked as carefully as the old one from the first cell onward.
Cybernetik has been building automation for more than three decades. It is headquartered in Pune with facilities in Gujarat and Raigad and offices in the United States and UAE, and has installed over 6,000 systems in more than 30 countries, including over 400 custom robotic solutions. Battery work has been delivered for manufacturers including Hero MotoCorp, TVS Motor, Livguard and Matter. More background is on the Cybernetik about page.