Key takeaways
Material handling is everything that happens between the steps that add value. Nothing is mixed, cooked, ground or packed while material is being moved, and yet in most plants a substantial share of labor, injury exposure and product loss occurs during exactly those movements.
That makes it an unusual target for automation. There is no output improvement to point at, because handling does not produce anything. What it does is determine how much of the plant capacity the value-adding equipment actually gets to use, and how much material arrives at each stage in the condition it should be in.
This guide looks at handling across the whole material flow rather than at any single machine, and at where the efficiency genuinely comes from.
The Hidden Cost: Counting Touches
The most useful audit in material handling takes an afternoon and requires no instruments. Follow one ingredient from the loading dock to the process and count how many times a person lifts, carries, opens, tips or decants it.
A typical sack-fed operation looks like this. Pallets are broken down, sacks are moved to a trolley, the trolley is taken to the charging point, sacks are lifted onto a platform, each is slit open, tipped into a hopper, and the empty bag is disposed of. That is around five separate lifts of a 25 kg sack.
Now scale it. A plant charging 500 kg per batch from 25 kg sacks handles twenty sacks per batch. At six batches a day that is 120 sacks. Three tonnes of material, lifted five times each, is fifteen tonnes of manual lifting per day.
Every one of those touches carries the same set of costs: labor time, a musculoskeletal injury exposure, an opportunity for dust release, an opportunity for foreign material to enter, and a chance for the wrong sack to be tipped into the wrong hopper. Automation in material handling is mostly about removing touches, and the touch count is the number that makes the case.
The Material Flow Lifecycle
Handling divides into six stages, and each has its own automation options and its own manual-handling burden.
| Stage | What happens | Automation options | What it removes |
|---|---|---|---|
| Intake | Material arrives in sacks, bulk bags, drums or by tanker | Bag tipping stations, bulk bag dischargers, slitters, depalletizers | The heaviest manual lifting and the dustiest task in the plant |
| Storage | Material is held between delivery and use | Silos for single products, IBCs for multi-product campaigns | Repeated decanting and floor space consumed by sacks |
| Conditioning | Caked material is restored, foreign matter removed | Lump breakers, sifters, magnetic separation | Hand-breaking lumps and screen blinding downstream |
| Transfer | Material moves between stages | Screw, belt, vibratory and bucket conveying, pneumatic transfer | Trolleys, buckets and manual carrying between machines |
| Feeding and dosing | Measured quantities enter the process | Metering valves, loss-in-weight feeders, weigh hoppers | Manual weighing and the giveaway that comes with it |
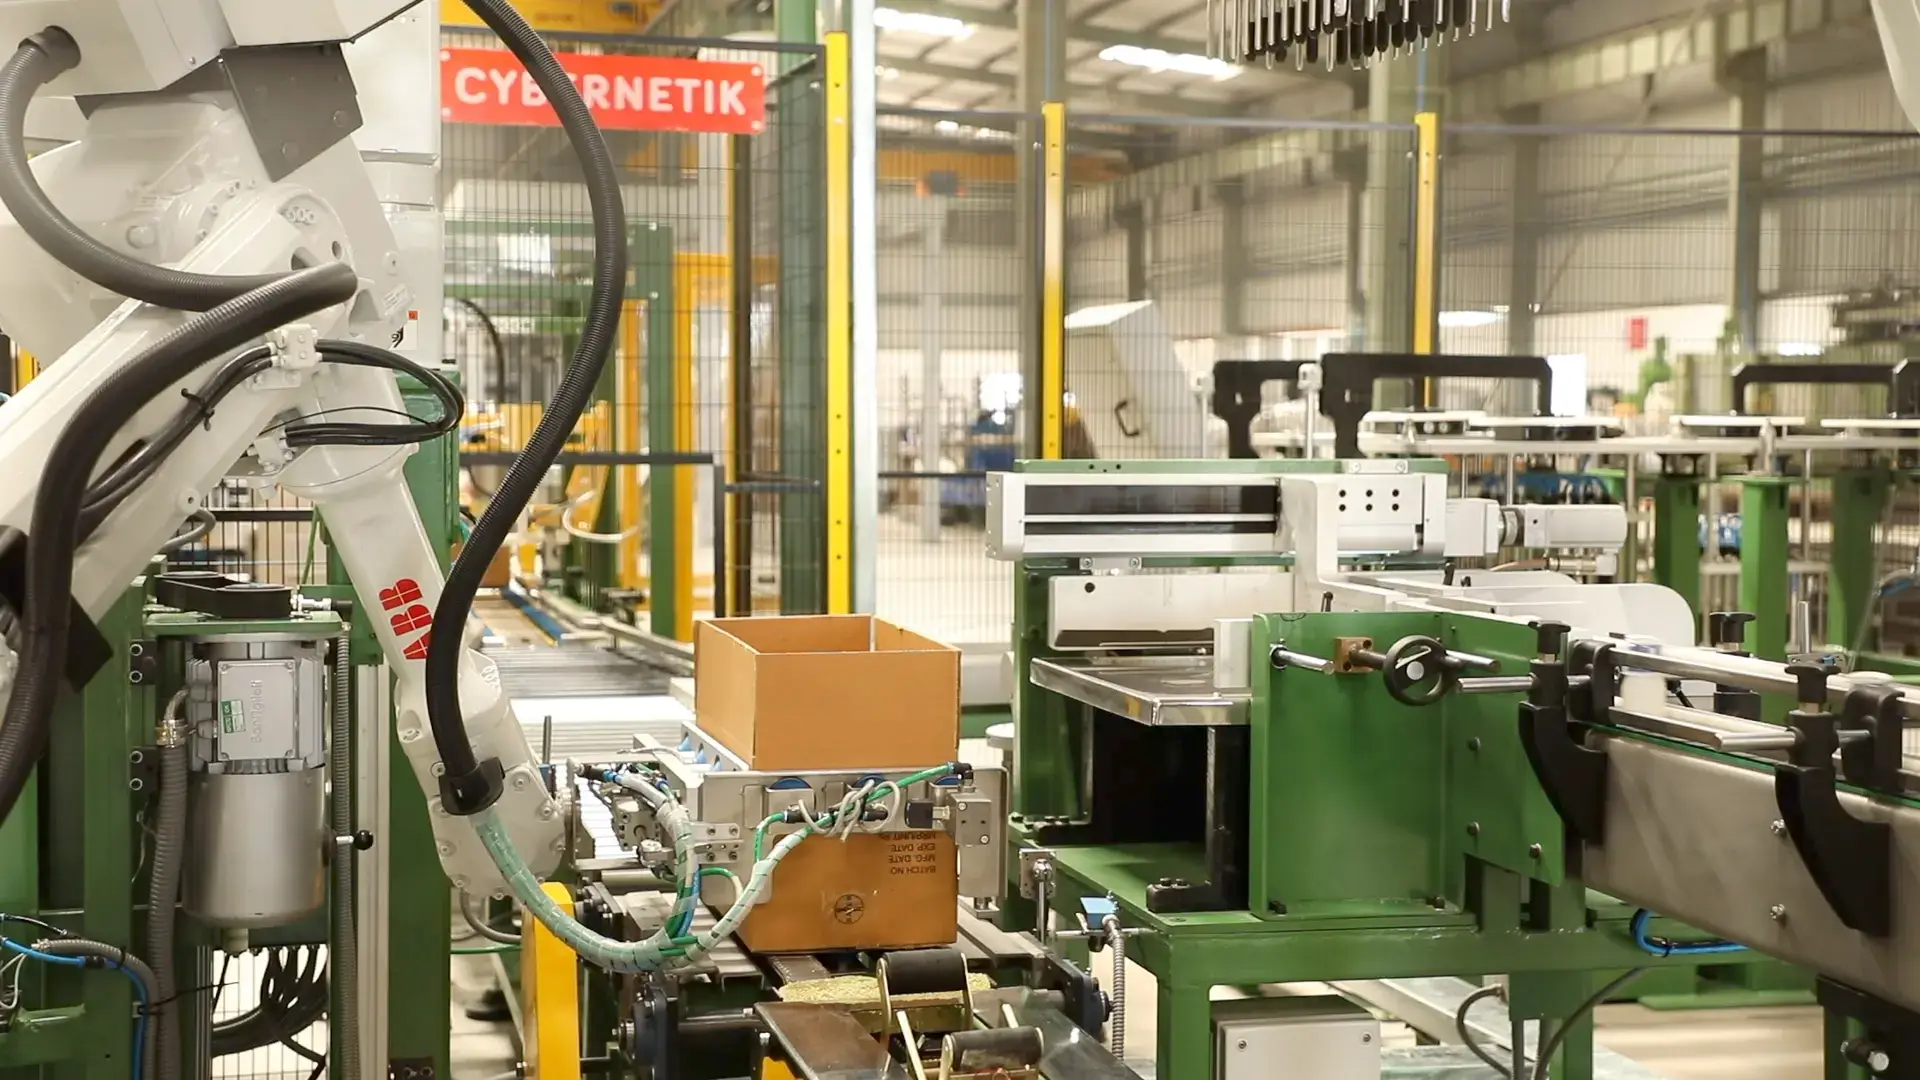
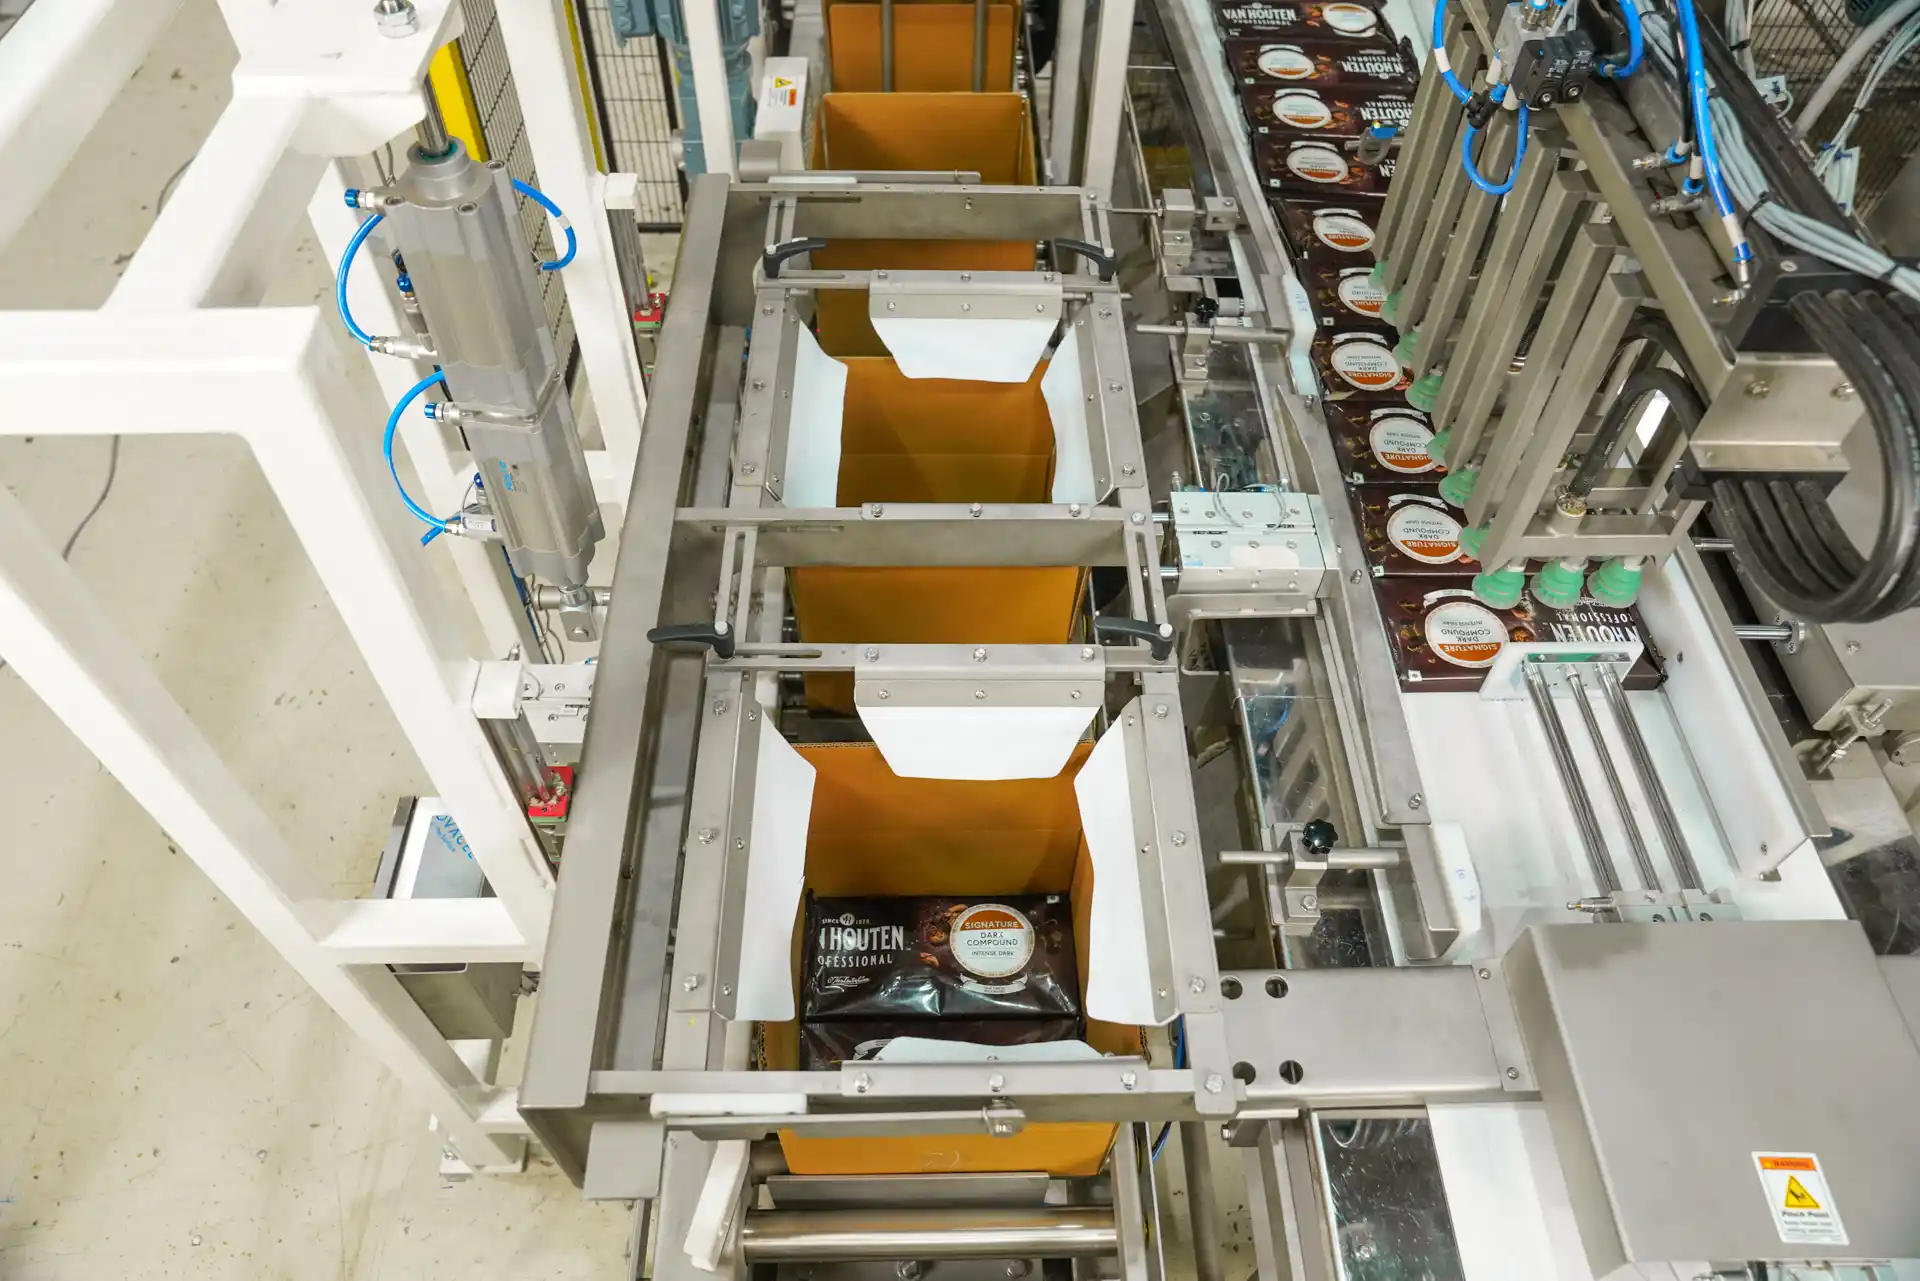
| Discharge and packing | Finished material leaves the process | Bag filling, weigh and fill, palletizing | Manual filling, weighing and stacking |
Two observations about that table. The heaviest manual work concentrates at intake and at packing, the two ends, because that is where material changes container. And the middle stages, conditioning, transfer and dosing, are where quality is protected rather than where labor is saved, which is why they are frequently justified differently.
Intake: Where Manual Handling Concentrates
If a plant automates one part of material handling, this is usually where the return is largest.
Sack handling is the most physically demanding routine task in most process plants and the dustiest. A bag tipping station with integrated dust extraction removes the dust exposure, and a magnetic grill at the tipping point removes tramp metal before it reaches any downstream equipment, which protects mills, valves and pumps rather than just improving housekeeping.
Moving up from sacks changes the arithmetic entirely. Bulk bags hold twenty to forty times as much as a sack, so a bulk bag discharger with contained docking replaces dozens of manual lifts with one forklift movement. Where a plant has the volume to buy in bulk bags rather than sacks, the handling saving frequently exceeds the material price difference.
Automated slitting and depalletizing takes it further, handling palletized sacks through to discharge without a person lifting anything. That suits high-volume single-ingredient intake, and it is harder to justify where deliveries are varied and infrequent.
Storage and Buffering
The storage decision follows from product variety rather than from volume.
A single product at high volume belongs in a storage silo, which removes packaging entirely and allows tanker delivery. Many products in campaign runs belong in intermediate bulk carriers, where each batch keeps its own vessel and segregation is managed by washing rather than by flushing shared pipework.
The handling advantage of IBCs is worth drawing out, because it is not obvious. Material is charged into the container once, and from then on the container itself moves through the plant. It can be lifted, docked over a mixer, blended while sealed, discharged and weighed without the powder being exposed or decanted again. That converts several touches into none.
Conditioning: Protecting What Comes Next
Material that has been stored arrives different from material that was just made. It cakes, it picks up moisture, and it occasionally contains things it should not.
Lump breaking and sifting at intake are cheap insurance for everything downstream. Lumps blind sifter screens, jam rotary valve rotors and survive mixing intact, so a batch fails uniformity for a reason the mixer cannot fix. Foreign material reaching a mill damages the mill and contaminates the batch.
The order matters. Magnetic separation belongs before lump breaking, so tramp metal is removed rather than broken up and distributed. Sifting belongs after, to catch whatever neither prevented.
Transfer: Choosing the Technology
Transfer is the stage with the most options and the one most often decided by habit. Belt conveying is versatile and open; screw conveying is enclosed and can take multiple inlets and outlets along its length; vibratory conveying is gentle and can screen or cool in transit; bucket elevators handle vertical lift in a small footprint. The comparison across types, and how they behave as a network, is covered in the guide to industrial conveyor systems.
The handling-specific point is that every transfer between conveyors is a place where material can spill, degrade or be exposed. Reducing the number of transfers is therefore a handling improvement as well as a reliability one, and a route spanned by one machine rather than three is better on both counts.
Feeding and Dosing
This is where handling automation stops being about labor and starts being about money in the product.
Manual weighing produces variation, and variation in a dosed ingredient means either a formulation that drifts or an operator adding margin to stay above minimum. Metered discharge under variable speed control replaces judgment with a rate, and coarse-and-fine staging lands on a target weight quickly without overshooting.
The accuracy figures matter here because they translate directly. A valve holding 0.1 percent on a dosed ingredient, against a manual process that overshoots by a percent or two, recovers material on every batch of every product.
 “Every manual touch creates another opportunity for labor loss, dust exposure, contamination, product waste, or handling errors; automation removes those risks by engineering the material flow as one connected system.“
See it in action
Containment and Dust
Enclosed handling is usually presented as a housekeeping benefit and is really four benefits at once.
Where the material is a combustible dust, ATEX rated construction and dust-free operation are specification items across the whole handling chain rather than at one station, since containment is only as good as its weakest point.
Where the Efficiency Actually Comes From
Common Mistakes
Four patterns recur in material handling projects.
Automating transfer while leaving intake manual. The heaviest work is at the ends, so automating the middle produces a plant where operators still lift every sack and the conveyors run empty waiting for them.
Buying containers without the handling equipment. IBCs without a column lift, a wash system and docking stations are expensive stainless vessels moved by hand, which is most of the cost and little of the benefit.
Sizing on average rather than on surges. Intake is inherently intermittent, since sacks and bulk bags arrive in bursts. Equipment sized for average throughput stalls on every delivery.
Treating containment as extraction. Extracting dust after it has escaped is more expensive and less effective than not releasing it, and it does not address the material already lost.
Material Handling from Cybernetik
Cybernetik builds material handling as complete lines rather than as individual machines, covering intake, storage, conditioning, transfer, dosing and packing under one control architecture. The full range sits under process automation solutions.
| Cybernetik material handling equipment | Specification |
|---|---|
| Bag tipping station | Manual sack emptying with magnetic grill for foreign particle removal |
| Big bag unloading system | Contained discharge of bulk bags into downstream process |
| Bag slitter and depalletizer systems | Automated opening and emptying of palletized incoming sacks |
| Intermediate bulk carriers | 30, 100, 500, 1,000 and 2,000 liters, SS304 or SS316, no dead zones |
| IBC column lift | Lifting and docking of IBCs up to 2,000 liters with position retention on power loss |
| Storage silo | 1 to 50 cubic meters, with integrated screw discharge to 6,000 kg/hr |
| Lump breaker | Up to 6,000 kg/hr, ATEX version available |
| Sifting | Turbo sifter to 6,000 kg/hr, vibro sifter 100 to 5,000 kg/hr, mesh 7000 down to 40 microns |
| Conveying | Screw to 40 m and 10 tons/hr, belt, trough, cleated, vibratory and bucket elevators |
| Metering valves | Rotary, CT and combination valves from 1,000 to 6,000 kg/hr at up to 0.1 percent accuracy |
| Packing | Open-mouth bag filling to 4,500 kg/hr at 0.1 percent weight tolerance |
The breadth is what allows a touch count to be attacked end to end. A plant automating intake alone still hand-carries material to the mixer; one automating conveying alone still lifts every sack. Where one party specifies intake, storage, conditioning, transfer and dosing together, the manual handling can be removed from the sequence rather than moved along it.
Cybernetik has operated for more than three decades, is headquartered in Pune with additional facilities in Gujarat and Raigad and international offices in the United States and UAE, and has installed over 6,000 systems across 30 plus countries, including more than 400 custom automation solutions. With over 600 employees and divisions spanning Process Automation, Packaging Automation, CleanTech, Extraction, Labs and Defence, handling is specified with knowledge of the process it serves. Further background is on the Cybernetik about page.