Key takeaways
Put a battery module on a cold plate and it looks as though the two are touching. Under magnification they are not. Both surfaces are rough and neither is perfectly flat, so they meet at a scattering of high points while most of the interface is a thin layer of air.
Air is one of the better insulators available, at roughly 0.026 W/mK. That thin, invisible layer is the reason a pack can have an excellent cooling system and still run hot cells. Thermal interface material exists to fill it.
This piece covers what these materials do, the types in use, why the datasheet number most people compare is the wrong one, and why the real difficulty is getting the material onto the line consistently.
Why It Matters More Than It Looks
A cell that runs a few degrees warmer than its neighbors ages faster. As it ages its resistance climbs, which makes it run warmer still. Over years that small difference turns into the cell that limits the whole pack.
That makes thermal uniformity a service life question, and the interface layer is where uniformity is won or lost. A cell with a good thermal path and a cell with a void beneath it will diverge exactly the way two poorly matched cells do, a pattern covered in the article on cell sorting and grading.
There is a second job the material does quietly. It sits between cells at high voltage and a metal cooling structure, so it also has to insulate electrically. A thermal layer that conducts heat well and fails dielectrically is a short waiting for a reason.
The Types in Use
| Material | Form | Where it earns its place | The catch |
|---|---|---|---|
| Gap pad | Pre-cured sheet cut to shape | Simple geometry, low volumes, easy rework | Needs compression to conform, which loads the cells, and fixed thickness cannot absorb tolerance |
| Gap filler | Paste dispensed and cured in place | Variable gaps, high volumes, automated lines | Dispense control, cure time and void prevention become the process |
| Thermal grease | Non-curing paste in a very thin layer | Flat, rigid interfaces with tight tolerances | Can pump out over thermal cycles and is messy to apply at scale |
| Phase change material | Solid pad that softens at operating temperature | Thin bond lines where grease handling is unwanted | Needs a first heat cycle to wet the surfaces properly |
| Thermally conductive adhesive | Dispensed paste that cures structurally | Cell-to-pack designs where the joint carries load | Rework becomes effectively impossible |
| Graphite sheet | Thin anisotropic film | Spreading heat sideways across a cell face | Conducts well in-plane and poorly through thickness |
On high-volume automotive lines, dispensed gap filler has largely taken over from pads. The reason is tolerance. Cells, modules and housings all vary slightly, and a pad of fixed thickness either leaves a gap where the stack-up is thin or has to be crushed where it is thick. A paste flows into whatever space exists, which is exactly what a real assembly needs.
The Conductivity Number Is Not the One That Matters
Materials are marketed on thermal conductivity, and buyers compare them on it. What actually governs heat flow through a joint is thermal resistance, and resistance depends heavily on how thick the layer ends up.
Resistance through a layer rises with thickness and falls with conductivity. So a thinner layer of a modest material can outperform a thicker layer of a better one.
| Interface | Layer | Relative thermal resistance |
|---|---|---|
| Air gap | 0.1 mm at 0.026 W/mK | About 15 times the gap filler below |
| Gap pad | 1.0 mm at 3 W/mK | About 1.3 times the gap filler below |
| Gap filler | 0.5 mm at 2 W/mK | Baseline |
The gap pad in that comparison has fifty percent higher conductivity than the gap filler and still performs worse, because it is twice as thick. And the air gap, only a tenth of a millimeter, is worse than both by a wide margin. That is the whole case for these materials in one line: a thin layer of anything reasonable beats a thinner layer of air.
The practical lesson is to specify installed thermal resistance at the bond line thickness your assembly will actually produce, rather than choosing on the headline figure. Contact resistance at each surface adds to that, which is why surface condition matters too.
Properties Beyond Conductivity
Mass
This is the property most often underestimated. Gap fillers are dense, commonly two to three and a half grams per cubic centimeter, because the thermally conductive fillers are ceramics. Spread across a full pack that adds up to kilograms, and every kilogram costs range. Lower-density formulations exist precisely because of this, usually trading some conductivity to get there.
Compression force
Pads and some fillers push back when compressed. That force transfers into the cells and the housing, and on a large pack it is not small. Softer materials are kinder to cells and harder to handle.
Silicone content
Many gap fillers are silicone based, and silicones can release low molecular weight compounds that migrate across nearby surfaces. On a battery line that matters, because contamination on electrical contacts or surfaces due to be welded or bonded causes problems that are very hard to trace back to a thermal material. Several manufacturers specify silicone-free formulations in some parts of the pack for exactly this reason.
Long-term stability
A pack cycles thermally thousands of times. Greases can pump out of the joint, some materials dry and crack, and any of these slowly raises thermal resistance over life. Stability over aging is worth testing rather than assuming.
Fire performance and serviceability
Flame retardancy is expected in a battery pack. Reworkability is a design choice: a cured gap filler can usually be removed, while a structural adhesive generally cannot.
Getting It Onto the Line
Choosing the right material is the easier half. Applying it the same way to every pack is where most of the difficulty sits.
Dispense accuracy
Too little material leaves voids. Too much wastes an expensive, heavy material and can squeeze out into places it should not be. Dispense weight per part is the first thing to control, and two-component fillers add mix ratio accuracy on top.
Bead pattern and voids
How the bead is laid down decides whether air gets trapped when the module is pressed onto it. Beads that close into a ring can seal a pocket of air inside, and that pocket becomes a hot spot directly under a cell. Pattern design is engineering work, not a detail left to the dispense operator.
Surface condition
The material has to wet both surfaces to make good contact, and contaminated surfaces wet poorly. That is one reason surface preparation upstream matters for thermal performance as well as for welding, as discussed in the piece on plasma cleaning in cell preparation.
Equipment wear
The ceramic fillers that make these materials conduct heat are also abrasive. They wear pumps, valves and mixers faster than most dispensed materials do, so wear parts and maintenance intervals belong in the equipment specification rather than being discovered in the first year.
Open time and cure
A two-part filler starts curing once mixed. If the line stops, material sitting in the mixer or on a part keeps curing, which affects both the joint and the equipment. Line stoppages need a defined response for this.
 “As cell-to-pack architectures combine thermal management with structural bonding, thermal material application becomes a core manufacturing quality process rather than a secondary assembly operation.”
See it in action
Why the Interface Has to Be Verified at the Station
Once the module is in place, the thermal layer cannot be seen. End-of-line electrical testing does not measure it, and a void under one cell produces no symptom until that cell ages early in service.
That leaves process control at the point of application as the only real defense: dispense weight recorded per part, bead path confirmed, and those records written against the pack identity. It is the same principle that governs welds and barrier placement. Check the characteristic where it is created, because there is no later chance.
Cell-to-Pack Raises the Stakes
In a module-based pack the thermal layer is one component among many. In a cell-to-pack design, thermally conductive adhesive frequently does two jobs at once, moving heat and holding cells structurally in place.
That combination raises every requirement at the same time. Bond strength now matters alongside conductivity, voids are both a thermal and a structural weakness, and the joint can no longer be reworked. Getting dispensing right stops being about efficiency and becomes the core of pack quality.
How Cybernetik Handles the Thermal Layer
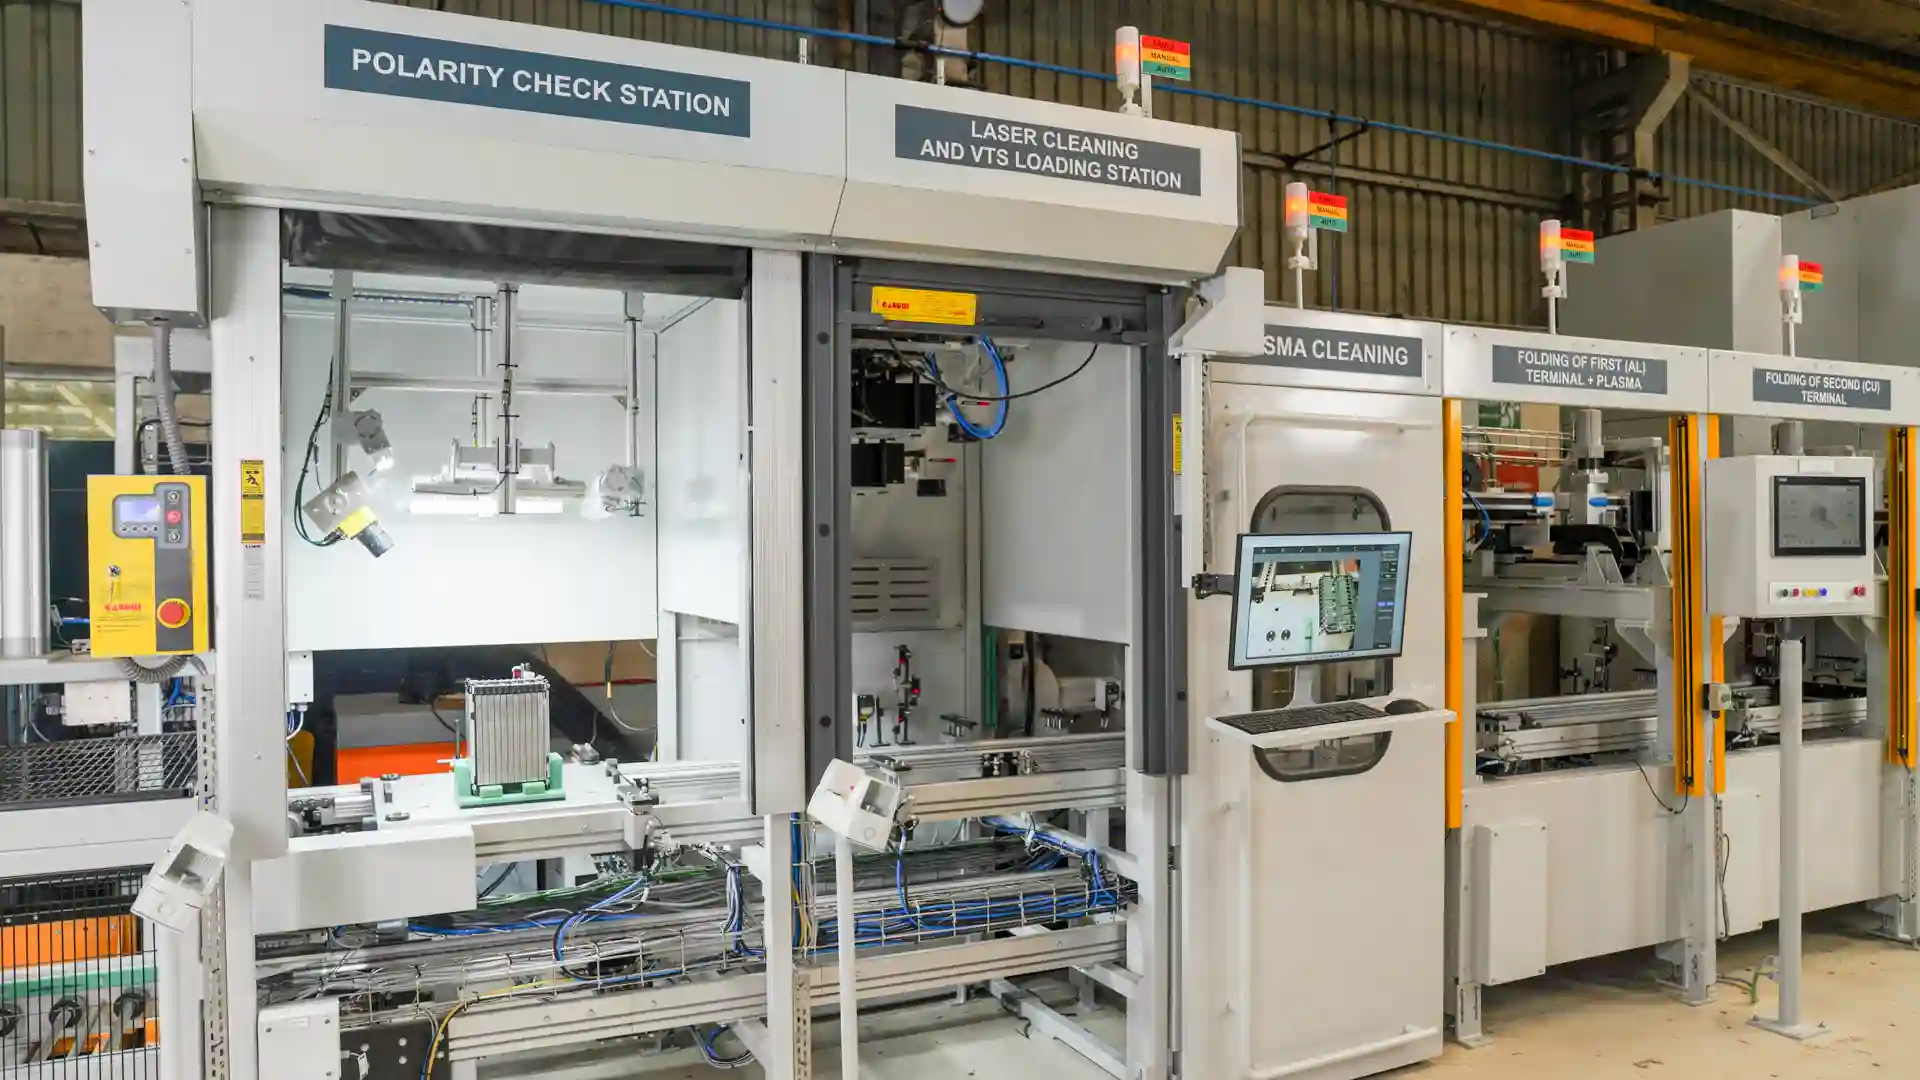
Thermal pad and Nomex sheet application is a defined station within the pack assembly zone of Cybernetik battery pack assembly automation, positioned before module insertion and cover closing so the layer is placed and confirmed while it can still be seen.
| Cybernetik pack assembly capability | Specification |
|---|---|
| Thermal layer application | Thermal pad and Nomex sheet application within the pack assembly zone |
| Pack assembly line | Pallet-based zone covering module insertion, temperature sensing, BMS mounting, gaskets and cover closing |
| Surface preparation | Plasma cleaning of cells within the cell-to-module zone |
| Temperature sensing | Dedicated station installing pack temperature sensors |
| End of line | BMS and TCU programming, air leakage testing, electrical testing and laser marking |
| Line rate | Up to 6,000 cells per hour through cell handling |
| Cell formats | Cylindrical 18650, 21700 and 32140, plus prismatic, pouch and blade |
| Traceability | Barcode and RFID capture with MES connectivity and process logging |
Two parts of that sequence connect directly to the points above. Plasma cleaning in the cell zone improves how surfaces take the thermal material as well as how they weld. And the pallet-based pack line holds each assembly in a repeatable position, which is what allows a thermal layer to be placed the same way on the thousandth pack as on the first.
Cybernetik has been building automation for more than three decades. It is headquartered in Pune with facilities in Gujarat and Raigad and offices in the United States and UAE, and has installed over 6,000 systems in more than 30 countries, including over 400 custom robotic solutions. Battery work has been delivered for manufacturers including Hero MotoCorp, TVS Motor, Livguard and Matter. More background is on the Cybernetik about page.