Key takeaways
A cell supplier calls to say one production lot may have a separator defect. Two questions follow immediately. Which of your packs contain cells from that lot, and where are those packs now?
A plant with working traceability answers both in minutes, with a list of serial numbers and customers. A plant without it answers in weeks, if at all, and usually ends up recalling far more than it needs to because it cannot draw a tighter boundary.
That gap between minutes and weeks is what traceability is really for. The rest of this piece covers how it actually works on a battery line, where the manufacturing execution system fits, and the practical failure points that leave gaps in an otherwise complete record.
Identity at Every Level
Traceability starts with every relevant item having an identity that can be read. On a battery line that happens at several levels, and they do not all work the same way.
| Level | Where the identity comes from | Typical marking | Tracked as |
|---|---|---|---|
| Cell | Assigned by the cell manufacturer | Code etched or printed on the cell | Serialized, one record per cell |
| Module | Created on the line when cells are grouped | Laser mark or label applied at build | Serialized, with its cells as children |
| Pack | Created on the line as the top-level unit | Laser mark applied after passing test | Serialized, with modules and components as children |
| BMS and electronics | Assigned by the board supplier | Board-level code | Serialized and paired to the pack |
| Busbars, gaskets, adhesives | Supplier lot or batch | Lot code on packaging or part | Lot tracked rather than serialized |
| Carrier or pallet | Assigned by the line | RFID tag on the fixture | Temporary link to whichever pack it is carrying |
The split between serialized and lot-tracked items is a deliberate choice. Cells, modules, packs and electronics are worth tracking individually, because each one carries its own measurements and can fail on its own. Busbars, gaskets and adhesives are usually tracked by lot, since what matters is knowing which batch went into which pack rather than which individual gasket.
The carrier row is the one people forget. On a pallet-based pack line, the pack is often awkward to scan at every station, so the pallet carries an RFID tag and the station reads that instead. The pallet is just a stand-in for whichever pack is sitting on it, which works well and brings its own risk, covered below.
Genealogy: The Parent and Child Record
Knowing each item’s identity is only half of it. The useful part is knowing how they relate.
When a cell goes into a module, the module becomes its parent. When a module goes into a pack, the pack becomes the parent of the module and, through it, of every cell inside. Each of these moments is a consumption event, and recording it builds a family tree for the pack that runs all the way down to individual cells and component lots.
That tree is what answers the recall question. It is also what carries the grade band a cell was sorted into all the way through to the finished pack, which matters because sorting only helps if the grouping survives assembly, as covered in the article on cell sorting and grading.
What the MES Actually Does
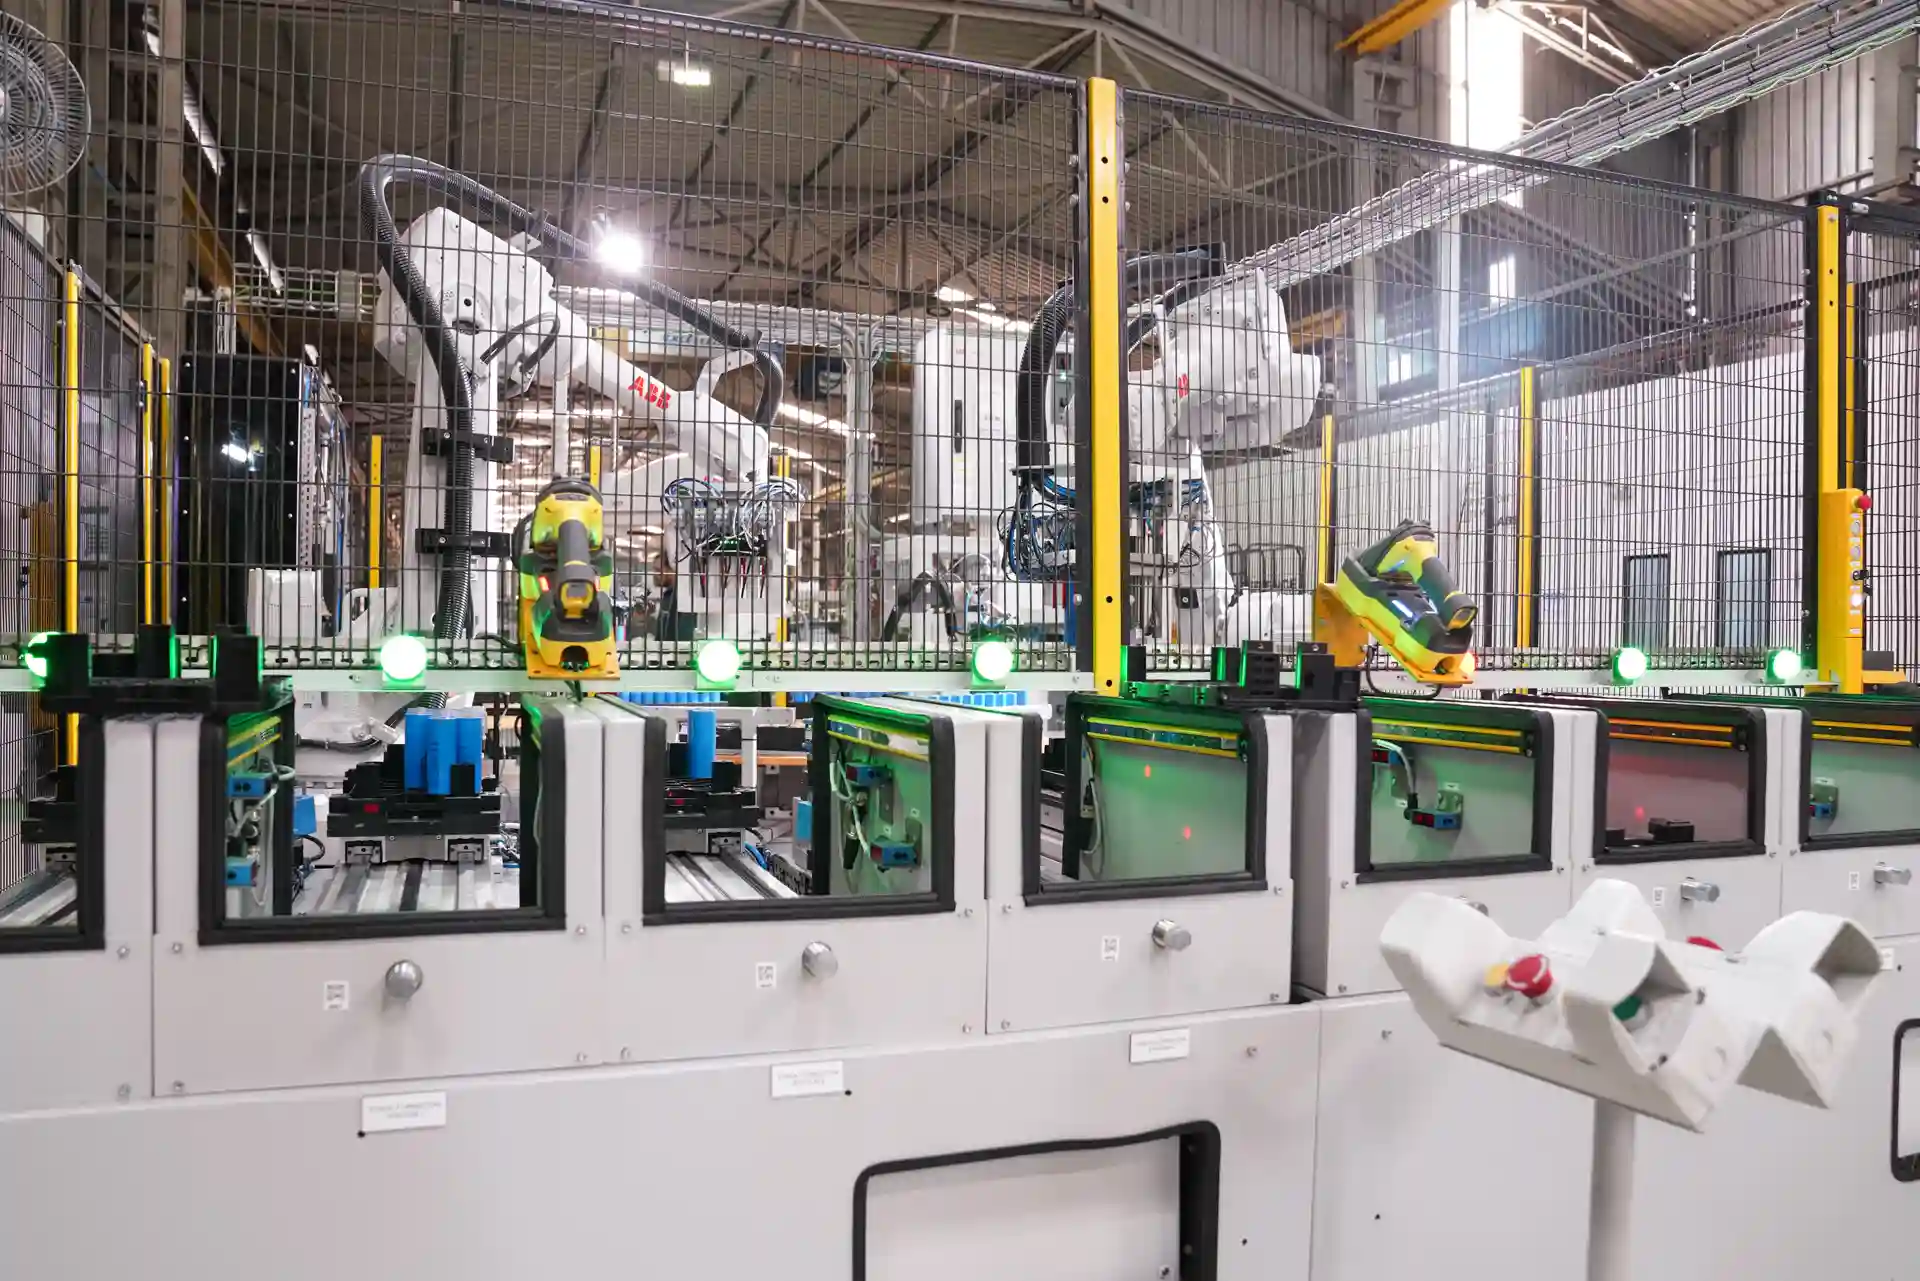
A manufacturing execution system sits between the machines on the floor and the business systems above them. On a battery line it does far more than store data.
| MES function | What it does on a battery line | What goes wrong without it |
|---|---|---|
| Route enforcement | Refuses to let a unit into a station until the previous step has passed | A failed part carries on down the line and gets built into a pack |
| Recipe download | Sends the correct parameters for the variant arriving at each station | The right hardware gets the wrong settings on a mixed-variant line |
| Data collection | Records measurements and results against the unit identity | Results live in machine memory and are overwritten |
| Genealogy | Links each child unit to its parent as it is consumed | Nobody can say which cells went into which pack |
| Rework control | Tracks removal, replacement and re-test of components | The record describes a pack that no longer exists |
| Work in progress view | Shows where every unit is and what state it is in | Bottlenecks and stuck units are found by walking the line |
The first row is the one that turns traceability from a record into a control. Without route enforcement, the MES can tell you afterward that a failed module was built into a pack. With it, the failed module simply cannot enter the next station, because the system knows its status and refuses it.
The Station Handshake
The mechanism behind all of this is a short exchange that happens every time a unit arrives at a station.
Every station on a traceable line runs some version of this. The details vary, but the principle is fixed: no unit gets worked on without being validated first, and no result exists without being written against the unit it belongs to.
Where Traceability Quietly Breaks
Most traceability systems look complete on paper. The gaps appear in a handful of predictable places.
Carrier marriage and divorce
When a pack is placed on an RFID pallet, the system links the two. When the pack leaves the pallet, that link has to end and transfer correctly. If a pack is lifted off for inspection and put back on a different pallet, or two pallets swap positions during a jam, the data from the next station is written against the wrong pack. This is one of the most common real sources of corrupted genealogy, and it needs deliberate handling at every point where a pack and its carrier can separate.
Unreadable codes
A cell code that will not scan presents a choice. Stop and deal with it, or let it through and lose its record. The line needs a defined answer, and the answer should never be that an operator types in whatever code seems right.
Manual stations
A station done by hand still has to record what it did. A traceability chain with one manual step that captures nothing is not a chain, it is two separate records with a gap between them.
Electronics pairing
The BMS carries its own identity, and it has to be written against the pack it sits in. Skip that step and the in-service data the BMS collects over the pack’s life never links back to how the pack was built. The pairing step is discussed in the piece on BMS integration on the assembly line.
Rework Without Breaking the Record
Rework is where a lot of genealogy quietly goes wrong. A module fails, a cell is replaced, the module is retested and passes. If the record still lists the original cell, it now describes a module that does not physically exist.
Handling rework properly means recording the removal of the old component, the fitting of the new one with its own identity, the retest result, and the reason for the change. It also means making sure removed components cannot drift back into normal stock. Rework is legitimate and often necessary; losing track of it is what causes problems.
 “BMS integration turns battery assembly into a controlled verification process, ensuring the right signals reach the right channels and every pack leaves production with a traceable identity.”
See it in action
When the MES Goes Down
Every connected system has outages, and a line needs a decided response rather than an improvised one.
One option is to stop the line whenever the MES is unavailable. That protects the record completely and costs production every time the network hiccups. The other is to let stations keep running and hold their data locally, then send it once the connection returns. That keeps the line moving, but only works if local storage is large enough, the data is timestamped reliably and the upload is confirmed rather than assumed.
Many plants use a mix: keep running through short interruptions with local buffering, stop if the outage goes past a set time. Whatever the policy, it should be written down, tested and understood by the people running the line, because the middle of an outage is a poor time to invent one.
Recall Queries That Actually Get Asked
It helps to design traceability around the questions it will need to answer, since those drive what has to be captured.
- Which packs contain cells from this supplier lot?
- Which packs were welded on this station between these two times, when the laser was later found out of calibration?
- Which packs used this batch of adhesive or this lot of gaskets?
- What were the build measurements for this specific pack that has just failed in the field?
- Which customers received the packs identified above?
Notice that some of those are about materials and some are about process conditions. A system that only tracks which parts went where can answer the first and third questions. Answering the second needs station, time and equipment data captured with each result, and answering the last needs the business system linked in as well.
Why This Is Now a Requirement
For a long time traceability was treated as good practice. It is becoming a condition of doing business, with digital battery passport requirements in the EU calling for serial-level identity and lifecycle information that only the assembly line can create. That shift is covered in the article on smart battery manufacturing.
The practical consequence is timing. Traceability that starts partway through a product’s life has no record of the units built before it began, and those early units are often the ones most likely to raise field questions. It has to be in place from the first pack.
How Cybernetik Builds It In
Cybernetik designs traceability into battery pack assembly automation from the first station rather than adding it once the line is running.
| Cybernetik traceability capability | Specification |
|---|---|
| Identity capture | Barcode reading at cell entry, with RFID through the assembly sequence |
| System connectivity | MES connectivity with process logging across stations |
| Cell records | OCV, IR and ACIR results written against each cell, with robotic sorting decisions recorded |
| Joint records | Weld integrity results for every joint on both module faces |
| Placement records | Insulation detection and polarity checking recorded per unit |
| Pack assembly | Pallet-based zone carrying each pack through module insertion, BMS mounting and cover closing |
| Electronics pairing | BMS programming and TCU mounting and testing tied to the pack |
| Release | Laser marking applied only after electrical and leak testing pass |
| Control architecture | Unified PLC and SCADA across stations |
The sequence is what makes the record usable. A cell is identified as it enters, its test results and sorting decision are written against it, the joints made to it are individually verified, and the pack it ends up in is only marked once it has passed testing. A single control architecture across all of those stations is what keeps the data joined up rather than split across machines that each keep their own records.
Cybernetik has been building automation for more than three decades. It is headquartered in Pune with facilities in Gujarat and Raigad and offices in the United States and UAE, and has installed over 6,000 systems in more than 30 countries, including over 400 custom robotic solutions. Battery work has been delivered for manufacturers including Hero MotoCorp, TVS Motor, Livguard and Matter. More background is on the Cybernetik about page.