Key takeaways
Conveyors are usually compared by how they work, belt against screw against vibratory, and that comparison is less useful than it appears. The more important division is what they carry.
A conveyor moving loose powder and a conveyor moving sealed cartons solve different problems, are specified against different criteria and fail in different ways. Almost every selection error in material handling comes from applying the logic of one to the other.
This guide starts from that split, covers the technologies on both sides of it, and sets out the questions that narrow the field.
Bulk Material or Unit Loads
Bulk material is loose and takes the shape of whatever contains it: powders, granules, flakes, aggregates. It has no discrete identity, so a conveyor handling it is judged on tonnes per hour, containment, degradation and how completely it discharges.
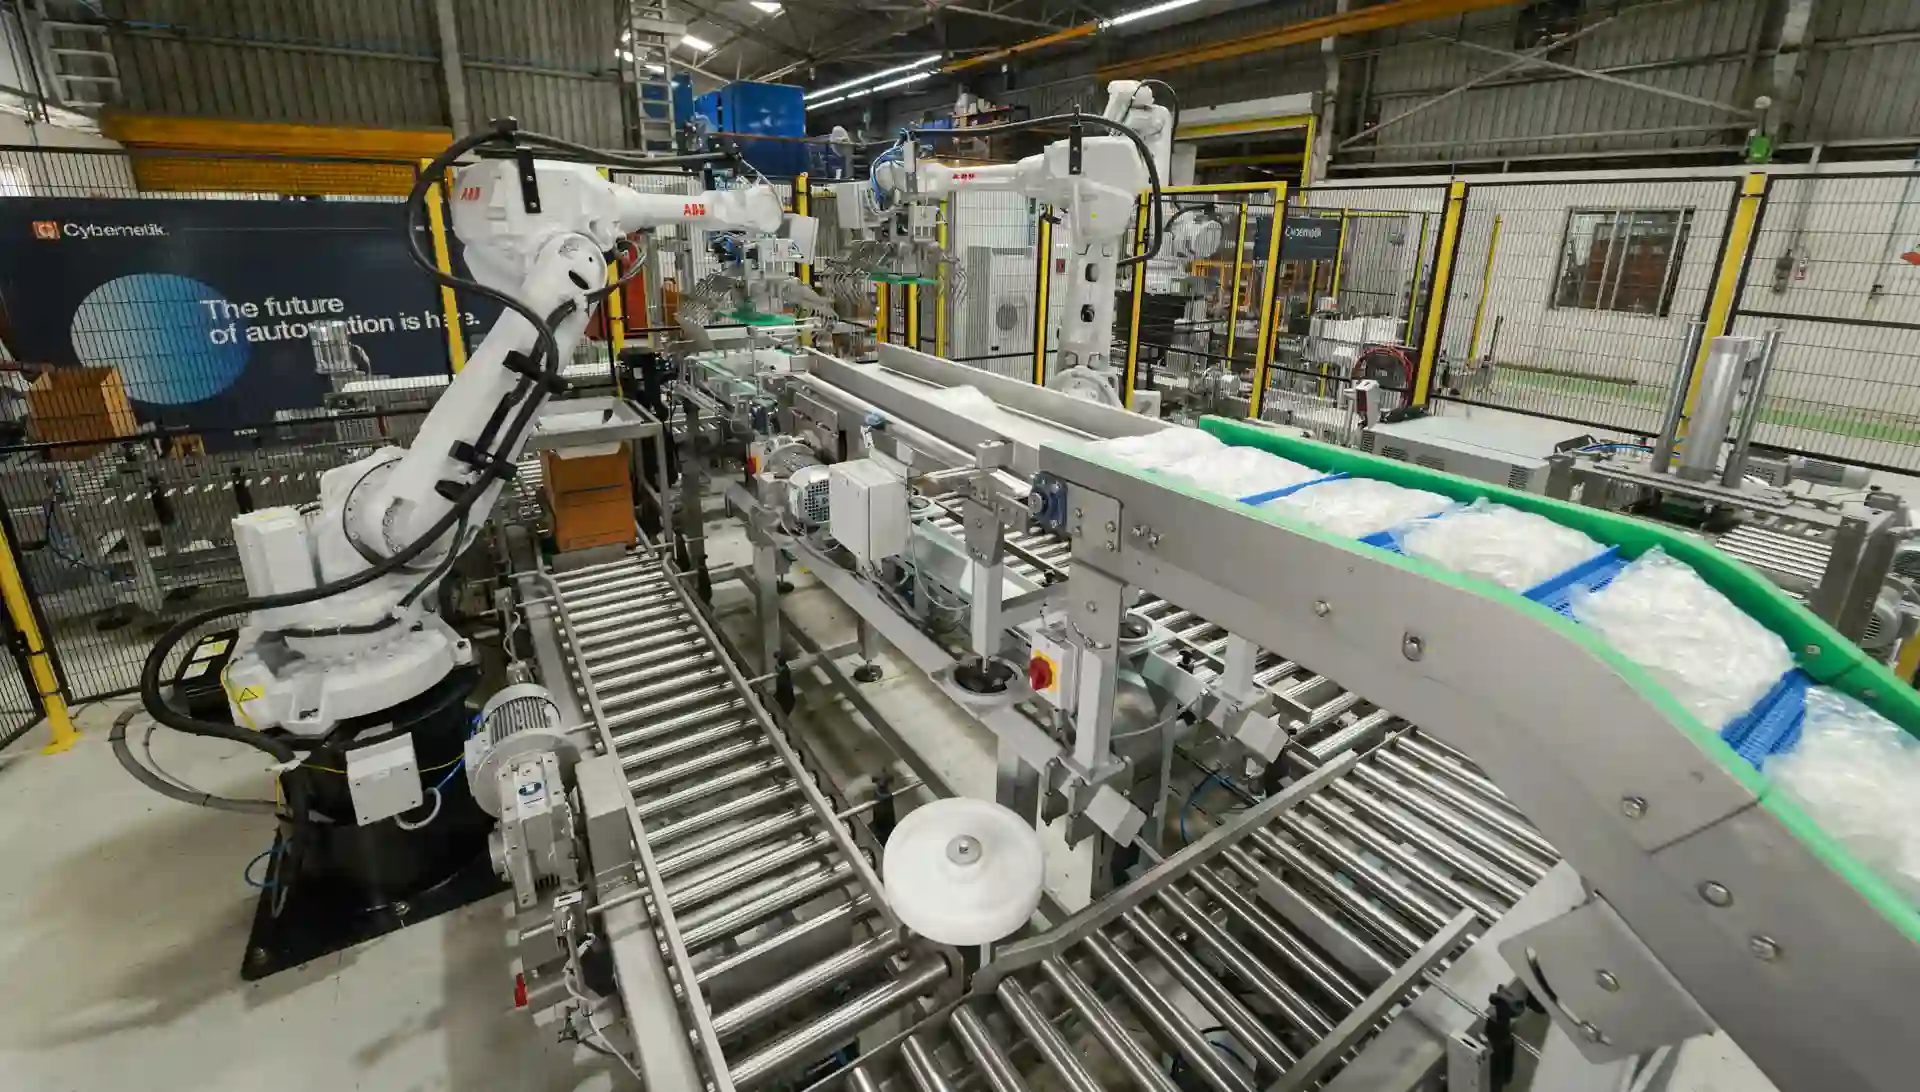
Unit loads are discrete items that keep their shape: cartons, sacks, trays, bottles, pallets. Each one is countable, so a conveyor handling them is judged on items per minute, orientation, accumulation and how gently each item is handled.
The consequences run through everything. Bulk conveying worries about dust, segregation and abrasion; unit handling worries about tipping, jamming and line pressure. Bulk conveying discharges continuously; unit handling frequently has to stop, hold and release. And the failure modes have nothing in common: a bulk conveyor fails by spilling or wearing, a unit conveyor fails by jamming or toppling loads.
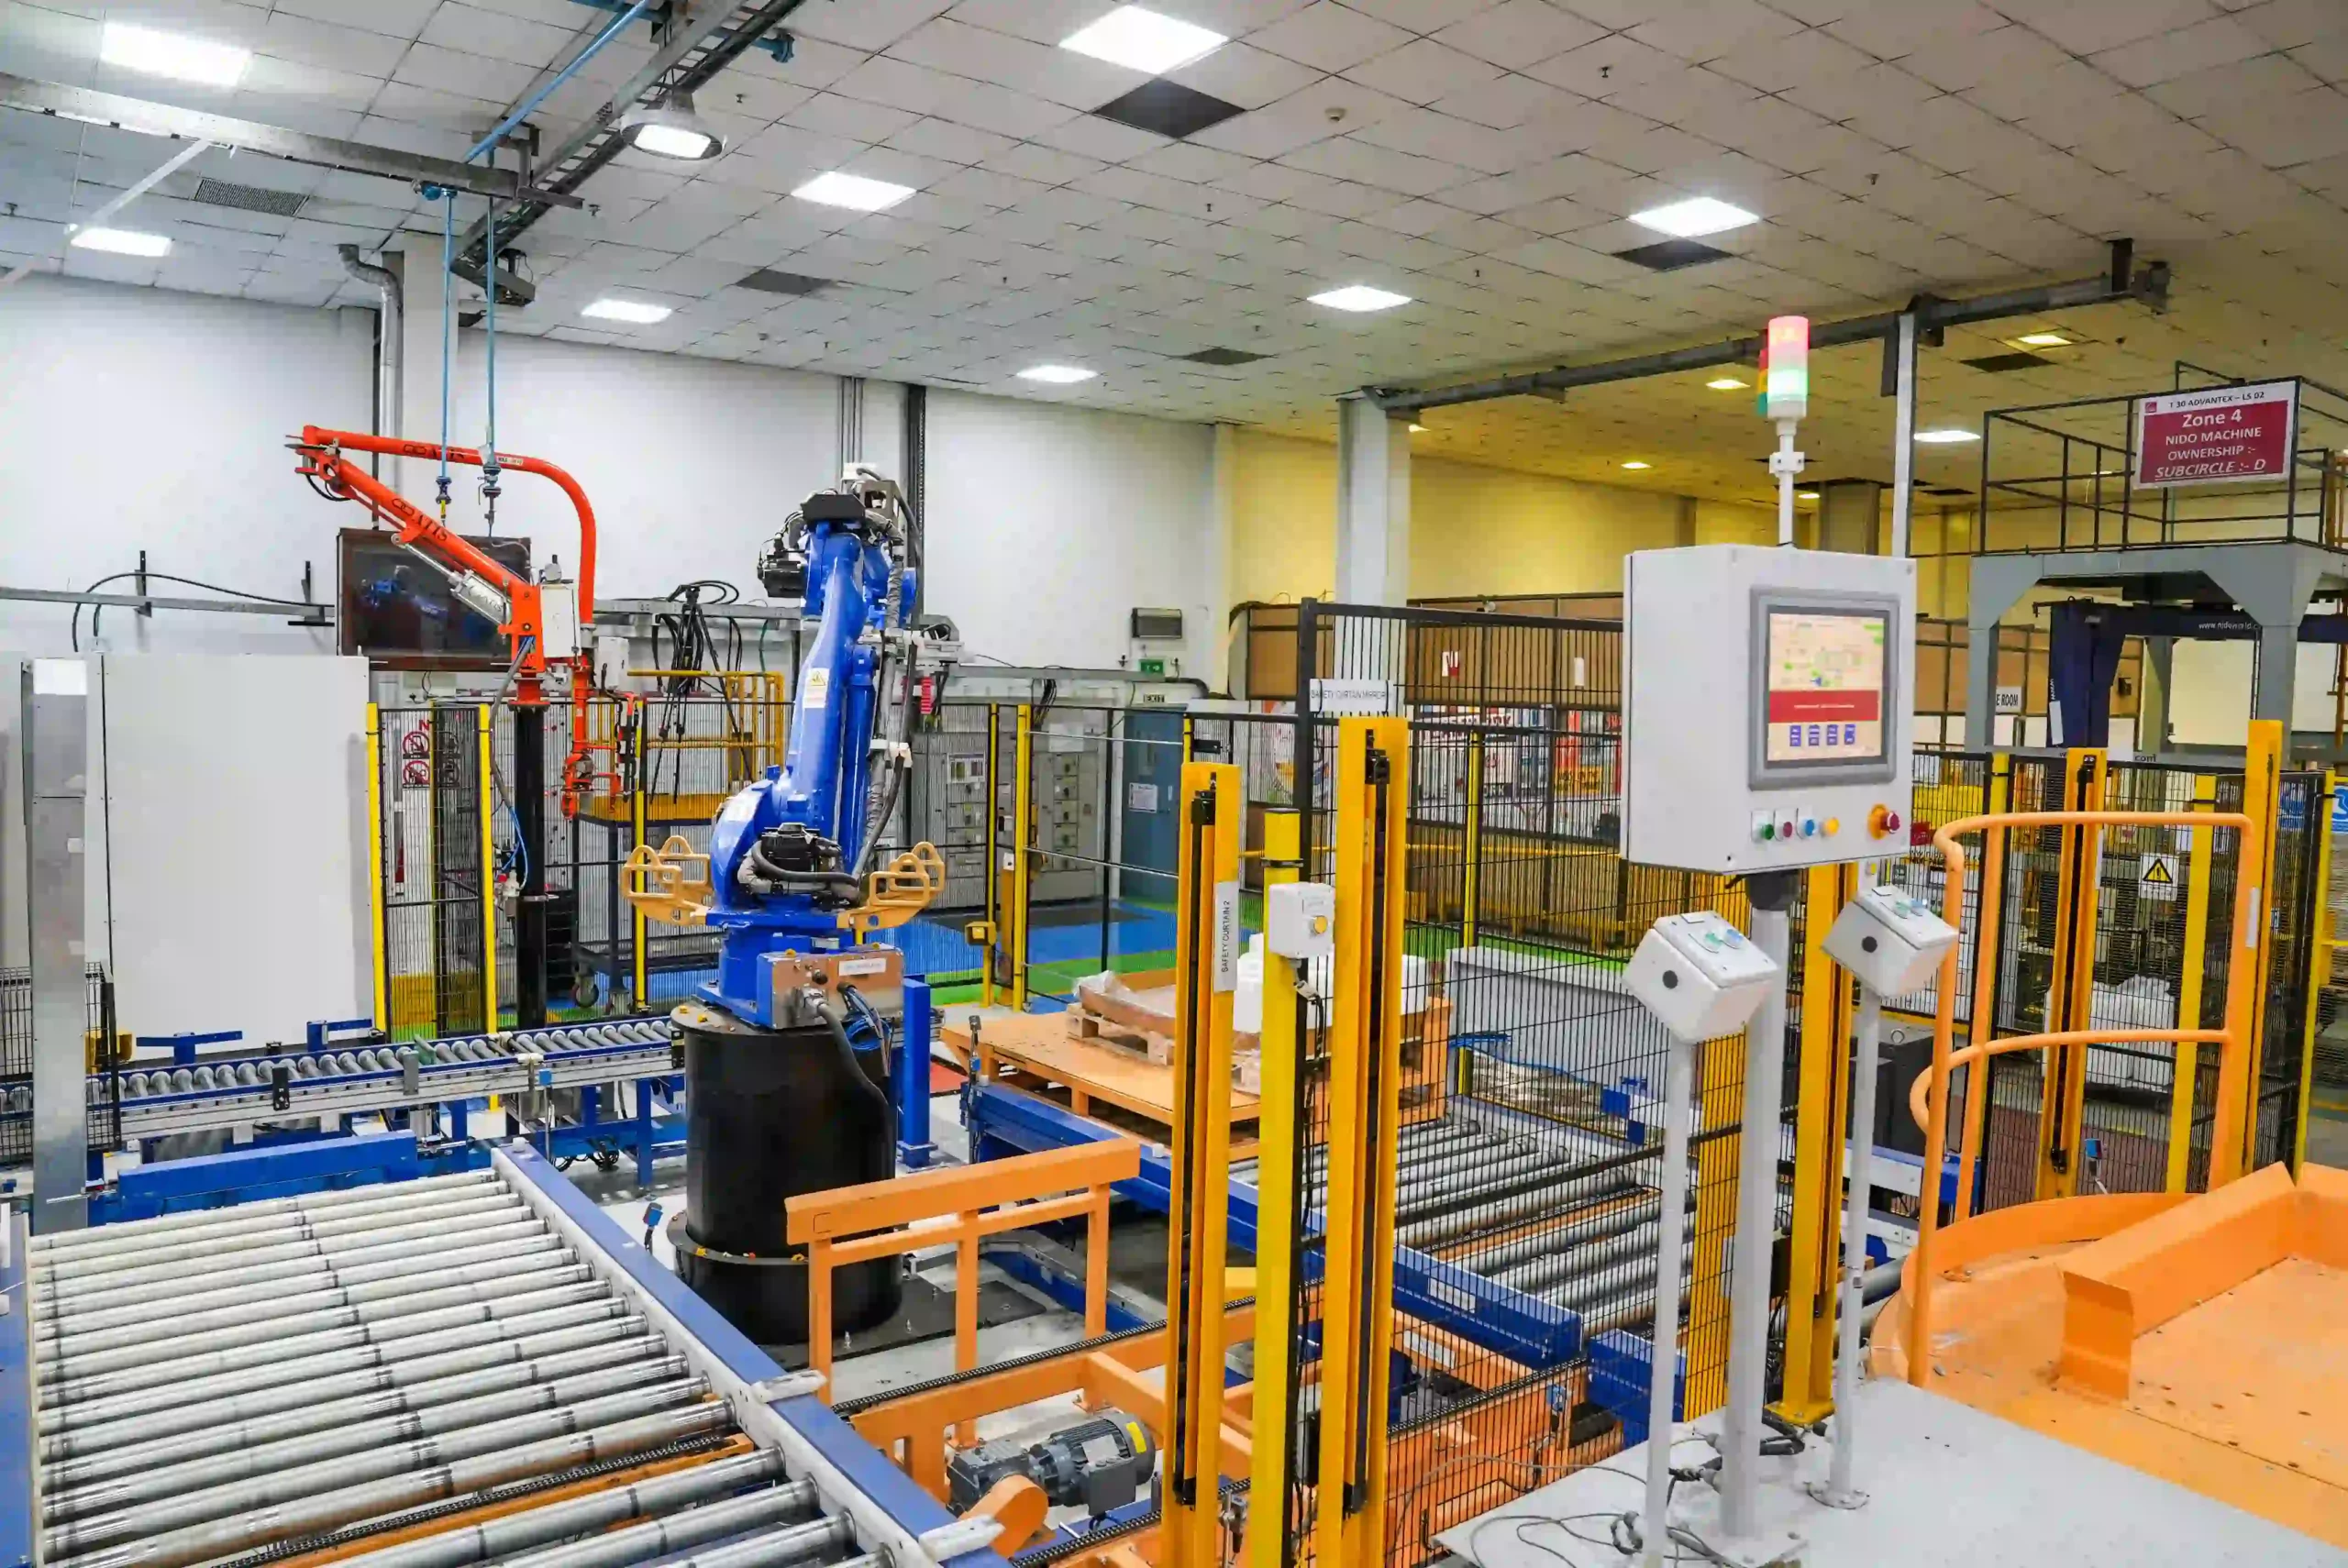
A plant almost always needs both, and the boundary between them is the packing line, where bulk becomes unit.
Bulk Material Conveyors
| Type | How it moves material | Strengths | Limits |
|---|---|---|---|
| Belt | Material rides on a moving surface | Long distances, high tonnage, low power per ton | Open surface, so dust escapes and contamination enters |
| Screw | A rotating flight pushes material along a trough or tube | Fully enclosed, multiple inlets and outlets, compact | Shears the product, wears with abrasives, capacity falls on inclines |
| Vibratory | Controlled oscillation moves material forward in small hops | Gentle, no belt to clean, can screen or cool in transit | Short distances, limited capacity, needs the right particle behavior |
| Bucket elevator | Buckets on a belt or chain lift material vertically | Substantial vertical lift in a very small footprint | Vertical only, and product is scooped and discharged |
| Drag chain | A chain with flights moves material en masse through a casing | Fully enclosed, gentle, high fill efficiency | Chain wear, and limited to relatively free-flowing material |
| Pneumatic | Air carries or pushes material through a pipe | Long routes, multiple destinations, complete enclosure | Blower, filter and receiver required; can degrade or segregate product |
Two entries in that table deserve more than a row. Drag chain conveying moves material as a mass rather than as a layer, filling the casing cross-section and moving it slowly, which makes it unusually gentle and efficient for the space it occupies. And pneumatic conveying is different enough in principle to warrant its own treatment.
Pneumatic Conveying
Air-based transfer sits apart from every mechanical option because the routing freedom it offers is not available any other way. A pipe can go around, over and through a building to several destinations, and adding a destination means adding a diverter rather than a conveyor.
It divides into two regimes that behave very differently.
Dilute phase
Material is suspended in a high-velocity air stream and travels as a cloud. The system is simpler, tolerant of a wide range of materials and cheaper to install. The cost is velocity: particles impact bends at speed, which degrades friable product and wears elbows, and fine material can segregate from coarse in transit.
Dense phase
Material moves at low velocity in slugs, pushed rather than carried, at higher pressure. Product damage and pipe wear fall sharply, and blends are far less likely to separate. The system is more complex, requires the material to behave suitably, and costs more to install.
The practical rule is that dilute phase suits robust, non-abrasive materials over moderate distances, and dense phase earns its cost where the product is fragile, abrasive or a blend that must stay blended.
What both share is that the conveying line is only part of the system. A blower, a filter receiver at the destination and a rotary valve at the feed point are all required, and their cost and footprint frequently surprise buyers who priced the pipe.
Unit Load Conveyors
Unit handling has its own technology set, and the governing question is usually not transport but accumulation.
| Type | How it works | Suits | Limits |
|---|---|---|---|
| Gravity roller | Free rollers on a slight fall carry loads by gravity | Short transfers, packing benches, loading docks | No speed control, and load must be stable and flat-bottomed |
| Powered roller | Driven rollers, often in independently controlled zones | Accumulation without pressure between loads | Cost per meter, and unsuited to unstable or small items |
| Belt | Loads ride on a continuous belt surface | Small, unstable or irregular items that rollers cannot carry | No accumulation without pressure unless zoned |
| Modular plastic belt | Interlocking plastic modules forming a belt | Curves, washdown environments, repair by module | Higher belt cost than a plain belt |
| Chain and slat | Loads sit on slats or directly on chain | Heavy loads, pallets, hot or oily conditions | Heavier construction and higher cost |
| Pallet conveyor | Roller or chain sized for pallet loads | Moving pallets between palletizing, wrapping and dispatch | Substantial structure and floor loading |
Accumulation deserves explaining because it decides more unit conveyor specifications than speed does. When a downstream machine stops, product continues to arrive, and what happens next depends on the conveyor.
On a plain belt, items pile against each other and the pressure builds through the queue, which crushes cartons, tips bottles and makes restart difficult. On a zoned powered roller conveyor, each zone stops when the one ahead of it is occupied, so items queue with a gap between them and no pressure at all. That difference is the reason zero-pressure accumulation exists as a category, and it is worth its cost wherever product is crushable or restart behavior matters.
 “A conveyor is only as effective as the system around it; transfers, feeding, accumulation, routing, and controls must be engineered together to achieve reliable material flow.“
See it in action
Questions to Put to a Supplier
Answering those six narrows most applications to one or two options. Capacity and price then choose between them, which is the reverse of how conveyor selection usually proceeds.
Applications
Where Selection Goes Wrong
Three patterns account for most of it.
Applying bulk logic to unit loads. A belt sized on tonnes per hour will move cartons perfectly well and provide no accumulation, no orientation control and no gentle restart, all of which the packing line needs.
Choosing on capital cost across technologies that are not comparable. An open belt is cheaper than an enclosed screw and does a different job. If containment is required, the belt was never an option, and comparing their prices is comparing a solution with a non-solution. This is the same reasoning set out in the guide to conveyor belt machines.
Specifying conveyors individually rather than as a network. Each machine can be correct and the system still perform poorly, because availability compounds across a chain and transfer points cause most of the problems. That behavior is covered in the article on industrial conveyor systems.
Conveying from Cybernetik
Cybernetik builds conveying across both categories as part of complete process and packaging lines, so the technology follows the material rather than the supplier position. Enclosed powder transfer uses screw conveying up to 40 meters and 10 tons per hour with multiple inlets and outlets, while gentle or dual-purpose duty uses vibratory conveying, which can screen or cool in transit.
Cybernetik has operated for more than three decades, is headquartered in Pune with additional facilities in Gujarat and Raigad and international offices in the United States and UAE, and has installed over 6,000 systems across 30 plus countries, including more than 400 custom automation solutions. With divisions spanning Process Automation, Packaging Automation, CleanTech, Extraction, Labs and Defence, bulk handling and unit handling sit in the same organization. Further background is on the Cybernetik about page.